Explore our primary export-grade, CE-compliant blister packaging capabilities engineered specifically for high-purity Beta Nicotinamide Mononucleotide (NMN), active nutraceutical ingredients, and custom solid dosage forms.
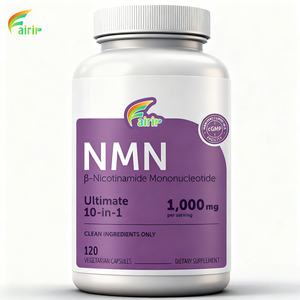
As global market demands for sensitive active pharmaceutical ingredients (APIs) and high-potency dietary supplements accelerate, selecting a validated CE certified blister packaging factory and exporter is critical to brand survival. Products containing moisture-sensitive compounds—such as 99% pure Beta-Nicotinamide Mononucleotide (NMN CAS 1094-61-7), NAD+ precursors, active enzymes, and probiotic strains—require specialized primary packaging solutions to mitigate oxidative degradation and hydrolytic loss.
Operating out of an advanced state-of-the-art facility audited under strict NSF/ANSI 455-2 GMP standards and registered with the U.S. FDA, our manufacturing plant integrates cleanroom thermoforming and cold-form aluminum blister lines with high-speed automated capsule filling (surpassing 5.5 million capsules daily capacity). By standardizing primary packaging protocols under ISO 15378 and European CE directives, we provide global brand owners, pharmaceutical distributors, and OEM buyers with fully traceable, retail-ready containment systems.
Our Utah facility complies with stringent NSF/ANSI 455-2 GMP regulations and European CE safety norms. Every production run undergoes rigorous identity, purity, and micro-particle validation to ensure zero cross-contamination.
Equipped with modern High-Performance Liquid Chromatography (HPLC) and Fourier-Transform Infrared Spectroscopy (FTIR), we verify raw material purity (e.g., 99% NMN assay) prior to encapsulation and blister sealing.
From custom ALU-ALU cavity tooling to tariff compliance, custom retail carton printing, and air/sea freight coordination, we manage full OEM export lifecycles for brands across North America, Europe, Asia, and the Middle East.
We engineer customized blister pockets utilizing Thermoformed PVC/PVDC, Aclar®, and Cold-Formed Aluminum foil (ALU-ALU) to achieve precise Water Vapor Transmission Rates (WVTR) under humid climate zones (Zone IVb).
High-speed camera inspection systems screen every individual blister cavity for micro-cracks, incomplete fills, capsule discoloration, and sealing defects before automated cartoning.
Whether launching market-validation pilot batches of 500 blister boxes or scaling up to multi-million unit monthly contracts, our flexible manufacturing workflow adapts to your growth strategy without quality compromise.
The global pharmaceutical and dietary supplement packaging industry is undergoing a paradigm shift driven by environmental sustainability mandates, anti-counterfeiting requirements, and heightened bio-availability retention standards. Procurement directors must align with factories capable of integrating next-generation material science.
Traditional PVC/PVDC multi-layer blisters present recycling challenges. Procurement trends are moving rapidly toward recyclable mono-polypropylene (PP) and high-density polyethylene (HDPE) thermoformed films that maintain moisture barriers while meeting European circular economy directives.
With high-value anti-aging molecules like NMN and longevity peptides prone to market counterfeiting, CE-certified exporters are incorporating micro-holographic foil printing, tamper-evident lidding, and unique QR serialization on individual blister cards for real-time consumer authentication.
As next-gen formulas incorporate hygro-sensitive plant extracts and co-enzymes, demand for zero-permeability Cold-Formed Aluminum packaging has grown by 14.8% annually. ALU-ALU provides total light, oxygen, and moisture exclusion, extending product shelf life up to 36 months.
Understanding the material science behind primary packaging formats allows brand owners to select the correct substrate for their specific formulation stability profile.
| Packaging Substrate | Moisture Barrier (WVTR) | Oxygen Barrier (OTR) | Light Protection | Ideal Application | CE & Global Compliance |
|---|---|---|---|---|---|
| Standard PVC (250µm) | Moderate (3.0 g/m²/day) | Low | Transparent / Low | Standard Vitamins & Non-hygroscopic powders | CE Compliant / Food Grade |
| PVC / PVDC (40g-90g) | High (0.6 g/m²/day) | Moderate to High | Medium Amber Options | 99% Pure NMN Capsules, Herbal Extracts | EU Regulation 10/2011 & FDA |
| Aclar® Laminated Film | Ultra-High (0.1 g/m²/day) | High | Custom Tinted | Highly moisture-sensitive APIs, Probiotics | US Pharmacopeia & CE Certified |
| ALU-ALU (Cold-Form Foil) | Near Zero (<0.005 g/m²/day) | Near Zero | 100% Opaque Barrier | Pharmaceutical Grade NMN, Enriched NAD+ | ISO 15378 / CE Medical Grade |
CE certification confirms that our blister packaging machinery, primary barrier films, and secondary cartoning systems comply with essential European safety, health, and environmental protection requirements (such as EU Directive 93/42/EEC and Regulation 2017/745 for medical and packaging compatibility). It grants seamless import clearances across the European Economic Area (EEA).
Nicotinamide Mononucleotide (NMN CAS 1094-61-7) is highly susceptible to hydrolytic degradation when exposed to ambient humidity. Every time a consumer opens a traditional bottle, the entire contents are exposed to air. Individual blister cavities isolate each capsule until the exact moment of consumption, preserving 99% purity and potency over extended shelf life.
For market-ready private label NMN formulas packaged in existing tooling formats, our MOQs start as low as 1,000 units. For fully customized blister cavity shapes, child-resistant push-through foils, or custom printed aluminum lidding, typical OEM runs begin at 5,000 to 10,000 retail boxes.
Yes. Our NSF/ANSI 455-2 GMP facility handles end-to-end processing—including bulk high-purity NMN powder sourcing, micro-dosing, capsule manufacturing (gelatin and vegetable HPMC shells), in-house label and folding carton printing, blister sealing, and export freight consolidation.
Every export shipment includes a full Certificate of Analysis (CoA) from an ISO 17025 accredited laboratory, Batch Production Records, Heavy Metal & Microbe Screening Reports, Stability Test Data, Certificate of Origin, and CE Compliance Declarations.
Standard private label blister packaging projects are completed within 2 to 3 weeks. Custom formulation, custom tooling engineering, and high-volume OEM contracts generally require 4 to 6 weeks depending on raw material testing and packaging proof approvals.
Consult with our senior packaging engineers and contract manufacturing specialists to receive instant pricing, custom cavity samples, and technical formulation reviews.
Contact Us