Explore our CE-certified, rapidly-dissolving effervescent catalog engineered for maximum bioavailability, superior taste profiles, and long-term active stability.
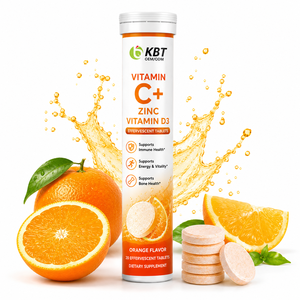
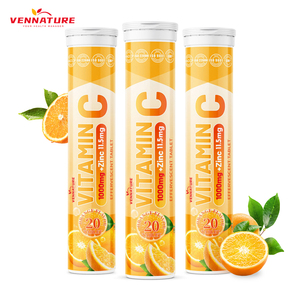
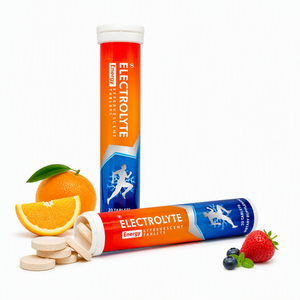
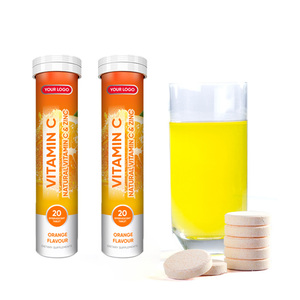
Effervescent delivery systems represent one of the most technologically demanding dosage formats in nutraceutical and pharmaceutical contract manufacturing. Unlike traditional swallowed tablets or hard capsules, an effervescent tablet relies on a precisely calculated biochemical reaction between an organic acid (such as anhydrous citric acid, tartaric acid, or malic acid) and an alkali carbonate or bicarbonate source (such as sodium bicarbonate, potassium bicarbonate, or magnesium carbonate).
When introduced to water, this system instantly liberates carbon dioxide gas ($CO_2$), creating a self-stirring micro-turbulent solution that fully solubilizes active pharmaceutical ingredients (APIs), vitamins, minerals, and botanical extracts within 60 to 180 seconds. This process not only accelerates gastrointestinal absorption but also neutralizes stomach acid irritation, offering superior bioavailability for sensitive compounds.
Effervescent formulations are exquisitely hygroscopic. Premature exposure to ambient humidity triggers localized acid-base reactions, compromising tablet integrity, dissolution kinetics, and active ingredient shelf-life. Our manufacturing plant operates under strict ISO Class 8 cleanroom environments with continuous HVAC dehumidification maintaining relative humidity (RH) below 20% and temperature controlled at 20°C ± 2°C throughout direct compression, fluid-bed granulation, and automated tube packaging.
| Performance Parameter | CE Certified Effervescent Tablet | Standard Swallowed Tablet | Hard Gelatin / HPMC Capsule |
|---|---|---|---|
| Disintegration Time | < 3 Minutes (Full Dissolution) | 15 – 45 Minutes | 10 – 30 Minutes |
| Gastric Tolerability | High (Buffered pH minimizes mucosal stress) | Moderate (Localized active concentration) | Moderate |
| Bioavailability Rate | Rapid Liquid-Phase Absorption | Delayed (Requires disintegration) | Medium (Requires shell dissolution) |
| Active Loading Capacity | High (Up to 2,000 mg per tablet) | Limited (~ 1,000 mg max) | Low-Medium (~ 700 mg max) |
| Environmental Control Needed | Strict < 20% RH HVAC Cleanrooms | Standard Humidity (< 45% RH) | Standard Humidity (< 45% RH) |
| Primary Packaging Requirement | Desiccant-Cap Aluminum/Plastic Tubes or ALU-ALU Strips | Blister Pack / HDPE Bottles | HDPE Bottles / Blister Packs |
Why leading global brands, pharmacy chains, and direct-to-consumer health companies partner with our US-based manufacturing operations.
Certified under NSF/ANSI 455-2 GMP for dietary supplements, FDA registered, USDA Organic certified via UDAF, and CE compliant for international markets across Europe, Asia, and the Americas.
Raw material identity verification via FT-NIR, HPLC potency assaying, heavy metal ICP-MS screening, and 100% batch records with retained reference samples for complete supply chain transparency.
Equipped with high-speed rotary tablet presses capable of producing over 5.5 million units daily, integrated with automated tube filling lines featuring inline desiccant cap insertion.
In-house flavor chemistry expertise specializing in masking bitter botanical actives (such as Shilajit, NMN, or high-dose minerals) with vibrant natural fruit systems including Orange, Berry, and Citrus.
From initial formula design and Supplement Facts panel compliance review to custom branding, container sizing, and retail-ready display box printing under a single unified project manager.
Battle-tested compliance workflows for Amazon Transparency, Walmart, Sam's Club, CVS, Target, GNC, and international customs import regulations (EU Directive 2002/46/EC).
As global consumers shift away from pill fatigue associated with traditional capsules and tablets, the market demand for functional, liquid-activated delivery mechanisms is expanding at an unprecedented compound annual growth rate (CAGR). Institutional buyers, brand managers, and procurement officers must align their sourcing strategies with several critical technological and market developments:
Modern consumers demand rapid hypotonic and isotonic fluid replenishment during high-intensity training. Standard hydration drinks often contain excess sugars and artificial preservatives. Next-generation effervescent electrolyte tablets combine sodium, potassium, magnesium, zinc, and bio-available trace minerals with zero-sugar natural stevia sweetener matrices, dissolving fast for instant cellular hydration.
Active longevity compounds such as Nicotinamide Mononucleotide (NMN), NAD+ boosters, Trans-Resveratrol, and Shilajit extracts are traditionally difficult to stabilize in liquid formats due to hydrolytic degradation. Effervescent tableting resolves this by keeping the dry active stable inside airtight desiccant tubes until the exact moment of consumption, maximizing bioactivity upon dissolution.
Beyond human nutrition, effervescent technology is revolutionizing eco-friendly home cleaning and detergent sectors. By concentrating cleaning surfactants, enzymes, and disinfectant actives into dissolvable effervescent tablets, brands eliminate 95% of single-use plastic water bottle shipping weights, drastically reducing carbon footprints and freight logistics overhead.
The primary technical barrier in manufacturing high-potency effervescent tablets lies in managing chemical reactivity during storage. Standard direct compression blending frequently leads to segregation, inconsistent dissolution rates, or soft tablets susceptible to capping. Our engineering facility utilizes advanced multi-stage processing:
By spray-granulating organic acids and alkalizing agent fractions separately using a micro-binder hydro-alcoholic solution, we create uniform spherical granules. This prevents premature reactions while ensuring rapid, vigorous effervescence upon contact with water.
Packaging integrity is non-negotiable. Our automated packaging lines press aluminum or food-grade polypropylene tubes sealed with specialized spring-loaded caps containing active silica gel or molecular sieve desiccants, continuously absorbing internal headspace moisture across a 24-month shelf life.
Essential guidance for procurement managers, brand founders, and quality assurance specialists sourcing effervescent products.
Our US manufacturing facility operates under full FDA registration and is audited and certified to NSF/ANSI 455-2 GMP (Good Manufacturing Practices) for dietary supplements. We also hold USDA Organic certification through the Utah Department of Agriculture and Food (UDAF), Natural Products Association (NPA) membership, and comply with European CE regulatory standards for export.
For catalog-ready private label formulations using established dies and flavor profiles, MOQs start as low as 1,000 to 3,000 tubes (10 to 20 tablets per tube). For custom contract formulations requiring bespoke active raw material sourcing and R&D pilot stability testing, production minimums generally start around 10,000 to 25,000 units per SKU.
All processing steps—from powder blending and fluid-bed drying to rotary tablet compression and primary tube packaging—occur in environmentally controlled ISO Class 8 cleanrooms equipped with desiccant HVAC systems that maintain relative humidity below 20% RH at a constant 20°C temperature.
Yes. We specialize in clean-label, sugar-free effervescent formulations utilizing high-purity natural stevia rebaudioside-M, erythritol, or monk fruit extract. Our formulation lab ensures superior taste profiles without artificial colorants or excess sodium burdens.
We provide comprehensive packaging solutions including rigid recyclable aluminum tubes, food-grade polypropylene (PP) tubes with desiccant caps, tamper-evident shrink sleeve banding, multi-tablet ALU-ALU strip blisters, and custom retail display boxes designed for shelf-ready merchandising.
Market-ready private label orders with pre-approved artwork typically ship within 3 to 4 weeks. Custom contract formulations take approximately 6 to 8 weeks, accounting for R&D formulation trials, analytical raw material testing, pilot batch compression, and finished-product CoA (Certificate of Analysis) release.
Yes. We assist global clients with full regulatory dossier preparation, including Certificates of Free Sale (CFS), Certificates of Analysis (CoA), stability testing reports under ICH climatic zone guidelines, quantitative ingredient breakdown lists, and allergen statements required for customs clearance in the EU, UK, Asia, and Latin America.
Absolutely. Beyond dietary supplements, our industrial tableting lines manufacture non-ingestible effervescent cleaning tablets, surface detergent kits, and glass cleaner refills designed for eco-friendly home care brands aiming to eliminate liquid shipping weight.