CE Certified Plant Protein Factory & Global Exporters

Industrial-Scale Enzymatic Hydrolysis, Non-GMO Isolate Extraction, & Turnkey OEM/ODM Private Label Manufacturing Solutions

CE Certified Plant Protein & Peptide Portfolio

High-purity, standardized plant protein isolates, hydrolysates, TVP, and custom nutritional formulas for global wholesale and private label brands.
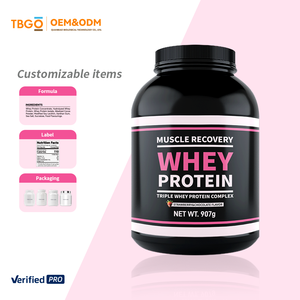
TBG 2025 OEM Mass Gainer Gym Isolate Drink Whey Plant Protein Powder

TBG 2025 OEM Musculation Supplement Fitness Muscle Body Fortress Weight Mass Gainer 907g Gym Isolate Drink Whey Protein Powder

Get Catalog
Textured Soy Protein TVP Vegan Meat Alternative

Vegan Food Textured Soy Protein High-Fiber Plant Protein for Sausages, Burgers for Southeast Asia Meat Alternative Industry TVP

Get Catalog
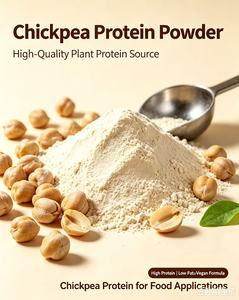
Chickpea Protein Plant-Based Isolate

Best Selling Chickpea Protein Plant-Based Protein

Get Catalog
Hydrolyzed Pea Collagen Protein Peptide Powder

Factory Supply High Quality Hydrolyzed Pea Collagen Protein Peptide Powder Bulk Pure Non-GMO Vegan Plant Extract Oligopeptides

Get Catalog
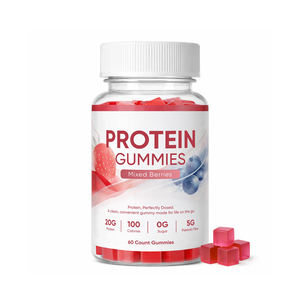
Plant Protein Gummies Vegan Protein

Wholesale Plant Protein Gummies Vegan Protein Mixed Berries Low Calorie Prebiotic Fiber Muscle Recovery Digestive Health

Get Catalog
Industrial Plant Protein Hydrolase Enzyme

Industrial Plant Protein Hydrolase Enzyme Proteolytic Enzyme Food Industrial Grade 99% Purity 5000 U/g Stable Performance Low

Get Catalog
Pea Protein Isolate 80% Food Grade Powder

Pea Protein Isolate 80% Food Grade Powder High Purity Non-GMO Water Soluble Vegan Plant Protein Wholesales 100%Plant Extract

Get Catalog
High Calcium Multi Peptide Protein Powder

High Calcium Multi Peptide Protein Powder, Plant Protein Nutrition Formula

Get Catalog
5.5M+
Daily Capsule & Packaging Output
80%+
Pea Isolate Protein Purity Ratio
NSF/ANSI
455-2 GMP Certified & FDA Registered
100%
Traceable Non-GMO Plant Ingredients

State of Global Plant Protein Sourcing & Advanced Bio-Extraction Standards

The global transition toward sustainable, allergen-friendly, and highly bioavailable macronutrient sources has shifted plant protein manufacturing from basic mechanical milling to sophisticated enzymatic hydrolysis and targeted peptide isolation. As a premier CE-certified plant protein factory and international exporter, our infrastructure addresses the stringent technological and regulatory demands of global food technology brands, pharmaceutical formulators, and sports nutrition enterprise buyers.

Traditional plant protein concentrates historically suffered from poor cold-water dispersion, anti-nutritional factors (such as phytates and trypsin inhibitors), and off-notes that compromised consumer acceptance. Modern bio-engineering has resolved these bottlenecks through controlled proteolytic enzymatic degradation, ultra-filtration membranes, and micro-encapsulation techniques. Consequently, ingredients like Hydrolyzed Pea Oligopeptides (PDCAAS = 1.0), Chickpea Protein Isolates, and High-Fiber Textured Soy Proteins (TVP) now match or exceed dairy-derived benchmarks in solubility, gelation, and branched-chain amino acid (BCAA) kinetics.

"Information Gain Insight: Modern enterprise buyers are migrating away from simple crude protein purity percentages toward Digestible Indispensable Amino Acid Scores (DIAAS) and molecular weight distribution profiles (< 1,000 Daltons for rapid peptide gut absorption)."

Our manufacturing complex incorporates end-to-end quality assurance systems compliance with NSF/ANSI 455-2 GMP standards, FDA registration, USDA Organic verification via UDAF, and comprehensive European CE compliance certification. By operating fully automated blending, enzymatic reaction vessels, vacuum drying towers, and cleanroom encapsulation lines, we ensure batch-to-batch consistency for over 115 market-ready formulations as well as complex custom contract manufacturing requests.

Vertical Integration & Processing Capabilities

From raw botanical sourcing to high-speed bottling and private label fulfillment, discover how our factory infrastructure mitigates supply chain friction.

Enzymatic Cleavage & Peptide Synthesis

Utilizing high-purity industrial plant hydrolase enzymes (5,000 U/g activity), we break complex botanical globulins into low-molecular-weight oligopeptides, eliminating bitterness while maximizing gut assimilation rates.

CE & ISO Global Compliance

Every export shipment is backed by heavy metal ICP-MS testing, microbial limits verification (<1,000 CFU/g), non-GMO documentation, and full CE sanitary certification for frictionless EU and global customs intake.

In-House Bottling & Label Printing

Consolidate your supply chain under one roof. We handle bottle selection, tamper-evident neck banding, Supplement Facts legal compliance review, and high-speed digital label printing without third-party delay.

Extrusive Texturization (TVP)

Our twin-screw thermal extrusion technology yields high-fiber Textured Soy Protein (TVP) and pea matrices with tensile fibrous structures tailored specifically for meat substitute burgers, nuggets, and sausages.

Hypoallergenic Formula R&D

Specializing in non-soy alternative isolates including high-solubility chickpea, pumpkin seed, water-soluble pea isolates (80%+ purity), and prebiotic-infused vegan gummies for gut health support.

Scalable Logistics & Bulk Container Shipping

From low-MOQ trial runs (300-1,000 bottles) for market validation to 20ft/40ft FCL bulk powder container shipments, our global export division manages ocean/air freight documentation seamlessly.

Future Sourcing Trends in Plant-Based Protein & Functional Peptides

As global buyers audit their raw material procurement strategies, key shift factors are redefining contract manufacturing criteria. Understanding these technical vectors ensures your brand remains competitive across Amazon, brick-and-mortar retail chains, and international pharmacy networks.

1. Molecular Weight Specificity in Hydrolysates

Nutraceutical brand owners are increasingly demanding enzymatic hydrolysis certificates specifying peptide length. Di-peptides and tri-peptides bypass normal digestive enzyme breakdown, entering blood flow intact via PepT1 transporters. Our plant hydrolase processing delivers stable 500–1,000 Dalton profiles for clinical nutrition applications.

2. Flavor Masking without Synthetic Additives

Consumer pushback against artificial flavorings has forced B2B suppliers to innovate natural bitter-blockers. Through clean-label pH adjustment and centrifugal debittering during wet extraction, our pea and chickpea isolates deliver clean, neutral taste profiles compatible with vanilla, berry, and unflavored formulations.

Furthermore, regional regulatory shifts—such as European Union micro-plastic constraints and North American heavy metal limits—require raw material suppliers to provide ICP-MS multi-element screening certificates with every batch. By integrating real-time inline particle size analyzers (maintaining mesh sizes between 80 to 200 mesh), our manufacturing plant guarantees rapid cold-water dissolution without gritty mouthfeel.

Frequently Asked Questions for Plant Protein Sourcing

Detailed technical, logistical, and compliance answers for quality assurance teams and procurement managers.

What specific certifications back your plant protein factory and export facility?
Our production ecosystem operates under strict NSF/ANSI 455-2 GMP certification for dietary supplements and is fully FDA registered. We maintain USDA Organic certification processed through the Utah Department of Agriculture and Food (UDAF), Natural Products Association (NPA) membership, and European CE alignment. All raw ingredients undergo 100% identity verification, heavy metal testing (Lead, Arsenic, Cadmium, Mercury), and microbiological screening before processing.
How does your plant protein hydrolase enzyme system improve product quality?
Our food-industrial grade proteolytic enzymes (99% purity, 5,000 U/g enzyme activity) break down complex plant globulins into highly bioavailable oligopeptides. This enzymatic hydrolysis process removes anti-nutritional compounds (phytates/tannins), dramatically improves cold-water solubility, reduces viscosity in RTD beverages, and accelerates intestinal amino acid absorption rates compared to raw protein concentrates.
What are the minimum order quantities (MOQs) for private label vs. custom contract runs?
For market-ready private label products utilizing our existing stock formulas (such as Pea Protein Isolate 80%, Vegan Gummies, or Mass Gainers), MOQs start at low unit volumes (typically 300 to 500 bottles per SKU). Custom contract manufacturing requiring unique blend formulations, specific flavor engineering, or custom extrusion parameters generally starts at 1,000 units for powders and 5,000 units for encapsulated or gummy products.
Can you manufacture both powder containers and encapsulated plant protein formats in one project?
Yes. Our Utah manufacturing plant houses high-speed encapsulation machinery capable of producing up to 5.5 million capsules daily alongside automated powder blending, canister filling, pouch sealing, and gummy packaging lines. Brand owners benefit from a unified project management team, single compliance audit, and consolidated export shipping.
What documentation is provided for ocean and air export clearance?
Every export order is accompanied by a full Lot Certificate of Analysis (CoA), Certificate of Free Sale (CFS), Allergen & Non-GMO Declaration, Heavy Metal & Pesticide Testing Report, Master Batch Production Record, and Harmonized System (HS) Code documentation matching destination country import requirements (e.g., EU, Southeast Asia, LATAM, Middle East).
How does Textured Soy Protein (TVP) perform in meat-alternative production lines?
Our High-Fiber Textured Soy Protein (TVP) undergoes controlled twin-screw thermal extrusion, creating an open fibrous matrix with exceptional water-holding capacity (3:1 hydration ratio) and oil-binding stability. It delivers authentic chewable meat textures for plant-based sausages, burger patties, and ready-to-eat minced products suitable for commercial food processing equipment.

Scale Your Plant Protein Brand with a Certified Manufacturer

Access 115+ market-ready formulas, custom R&D formulation, in-house label printing, and global export support from our NSF GMP certified plant.