Explore our top-tier bulk powders, encapsulates, and custom bottled solutions produced in certified cGMP packaging cleanrooms.
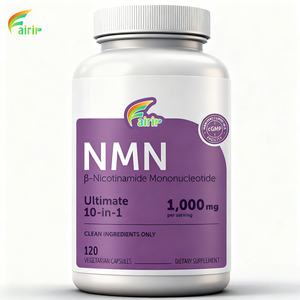
The global dietary supplement and contract packaging sector is experiencing a profound paradigm shift driven by semantic user intent, demand for absolute supply chain transparency, and stringent regulatory oversight. As international brand owners search for China Best Contract Packaging Factories & Suppliers, the strategic selection process has evolved from simple cost-per-unit negotiation into an analytical evaluation of technical compliance, analytical quality assurance (QA/QC), raw material traceability, and automated packaging agility.
China's manufacturing infrastructure for active pharmaceutical ingredients (APIs), nutraceutical powders, and specialized longevity compounds like Beta-Nicotinamide Mononucleotide (NMN CAS 1094-61-7) represents the backbone of the global anti-aging and health supplement industry. Modern contract packaging facilities in Eastern and Southern China now integrate automated bottling, high-speed encapsulation, blister Thermo-forming, and dual-facility international quality systems (such as NSF/ANSI 455-2 GMP and FDA registration). This whitepaper provides brand directors, procurement officers, and supply chain executives with a comprehensive blueprint for evaluating Chinese contract packaging partners, predicting procurement trends, and capitalizing on advanced technology.
From chemical synthesis and micro-milling to primary bottling, custom labeling, and global export packaging.
State-of-the-art cleanrooms equipped with optical tablet counters, induction foil sealers, automated capping, and nitrogen flushing capabilities for oxygen-sensitive materials.
Precision micro-dosing and blending of bioactive ingredients, NMN powders, collagen, and dietary proteins with tight particle size uniformity.
Rigorous analytical testing using HPLC, LC-MS, heavy metal ICP-MS, and microbiological cultures to ensure absolute purity and regulatory compliance.
The contract packaging industry in China is undergoing rapid modernization driven by technological advancements, environmental policies, and dynamic consumer preferences. To maintain a competitive edge, global procurement leads must understand the key structural shifts transforming supplier workflows:
1. Intelligent Anti-Counterfeiting & Serialized Traceability: Premium bioactive compounds such as 99% Pure NMN Powder (CAS 1094-61-7) are prime targets for marketplace counterfeiting. Top-tier Chinese contract packagers now embed unique QR codes, invisible UV security markers, and blockchain-enabled lot tracking directly onto bottle labels and outer cartons. This allows retail buyers and end consumers to verify ingredient provenance instantly via mobile scan.
2. Sustainable & High-Barrier Eco-Packaging: Regulatory mandates across Western markets are accelerating the transition away from single-use virgin plastics. Modern contract packaging factories in China are investing heavily in biodegradable PLA pouches, post-consumer recycled (PCR) PET bottles, and recyclable mono-material barrier foils. These eco-friendly solutions maintain zero moisture vapor transmission (MVTR) and oxygen protection—critical for preventing NMN oxidation.
3. Micro-Encapsulation & Targeted Delivery Formats: Beyond raw powder and standard hard-shell capsule encapsulation (HPMC veggie or gelatin), top suppliers offer specialized enteric coating, liposomal liquid-filled hard capsules (Licaps), and sublingual micro-tablets. These delivery systems significantly boost the bioavailability of active metabolites while preventing degradation in stomach acid.
4. Flexible Low-MOQ Validation Runs for DTC Brands: Recognizing the surge in direct-to-consumer (DTC) digital brands, advanced contract packaging suppliers have re-engineered their line setups. By leveraging quick-changeover automated bottling lines, factories can accommodate small-batch market validation runs (300 to 1,000 bottles) before scaling up to high-volume commercial runs exceeding 500,000 units.
Benchmark key operational metrics to ensure your supply chain avoids common quality pitfalls, customs holds, and label compliance rejections.
| Operational Evaluation Factor | Tier-1 Integrated OEM Packaging Factory | Low-Tier Packaging Workshop | Brand Impact / ROI Benefit |
|---|---|---|---|
| Quality System & Audit Status | NSF/ANSI 455-2, cGMP, ISO 22000, FDA Registered | Basic Local Business License Only | Guarantees seamless retail intake & zero customs seizures |
| Analytical QA/QC Testing | In-house HPLC, LC-MS, ICP-MS, Microbe Cultures | Visual inspection or outsourced unverified CoAs | Prevents active ingredient label claim under-dosing |
| Cleanroom Environmental Standard | Class 100,000 (ISO Class 8) HEPA-filtered cleanroom | Standard ambient warehouse packaging area | Eliminates cross-contamination & particulate pollution |
| NMN Pure Powder Handling | Dehumidified, temperature-controlled environment (<40% RH) | Unregulated humidity (risk of clumping/degradation) | Preserves 99%+ chemical potency & flowability |
| Turnkey Packaging Services | Bottling, Blistering, In-house Label Print, Outer Case Packing | Bottling only (requires external print vendors) | Reduces lead time by 3–5 weeks and lowers logistics costs |
| Traceability & Batch Records | Full Master Manufacturing Record (MMR) & Lot Retains | Incomplete batch logging | Ensures effortless audit defense & recall protection |
The rapid commercial adoption of Beta-Nicotinamide Mononucleotide (NMN) and NAD+ precursors highlights a broader shift in consumer purchasing behavior. Intent data reveals that end-users actively seek scientifically validated, high-purity longevity supplements over generic vitamin formulations.
To cater to this trend, brand owners sourcing from China contract packaging suppliers must implement multi-layer quality verifications:
High-Resolution Purity Assays (HPLC): Enterprise buyers must ensure every batch of NMN raw material demonstrates ≥99.0% purity via High-Performance Liquid Chromatography. Unrefined NMN synthesis can leave chemical byproducts, residual solvents, or heavy metals. Partnering with a contract packager that maintains strict raw material quarantine protocols guarantees that only premium-grade raw powders reach the packaging line.
Packaging Integrity for Hygroscopic Powders: NMN powder is extremely hygroscopic and sensitive to moisture absorption, heat, and air exposure. Contract packaging lines must utilize desiccant canisters, double-walled induction heat seals, and dark amber PET or glass bottles to mitigate hydrolytic breakdown over the product's 24-month shelf life.
Clear, direct responses to key operational and regulatory questions from international buyers.
Contact our senior technical sales team to discuss custom NMN formulations, sample requests, packaging dielines, and bulk pricing options tailored to your market.
Contact Us