Precision-engineered, NSF GMP certified, market-ready bulk dietary supplements available for private label customization and international export.
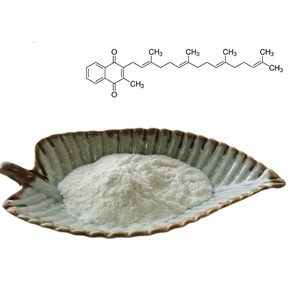
The global dietary supplement industry has entered an era defined by stringent analytical oversight, heightened consumer scrutinization of active ingredient purity, and intense margin pressures. Within this macroeconomic landscape, searching for a reliable China top bulk vitamins manufacturer is no longer merely a exercise in cost minimization—it is a critical supply-chain architecture decision. China currently manufactures over 70% to 80% of the world’s active pharmaceutical ingredients (APIs) and bulk vitamin premixes, including L-Ascorbic Acid (Vitamin C), Menaquinone-7 / Menaquinone-4 (Vitamin K2), Pyridoxine (Vitamin B6), Cyanocobalamin (Vitamin B12), and Cosmetic Retinol (Vitamin A Palmitate).
However, navigating the ecosystem of Chinese chemical synthesis plants, fermentation hubs, and contract packaging entities requires a sophisticated understanding of compliance frameworks, batch-to-batch analytical validation, and ingredient bioavailability. Overseas brand owners, pharmaceutical distributors, and retail brand aggregators face complex challenges regarding regulatory friction, Amazon dietary supplement compliance requirements, FDA 21 CFR Part 111 adherence, and supply chain transparency.
Core Procurement Insight: A top-tier Chinese contract manufacturer does not operate simply as a raw material vendor. Modern leaders integrate raw material chemical synthesis or bio-fermentation directly with downstream dose processing—such as micro-encapsulation, vegan pectin gummy cooking, liposomal powder spray-drying, and automated bottling under NSF/ANSI 455-2 cGMP environments.
By bypassing multi-layered middle trading houses and partnering directly with fully integrated manufacturing entities, brand owners achieve dual advantages: **maximum information gain regarding raw material origin** and **substantial cost-per-unit compression**. This whitepaper outlines the structural parameters of the bulk vitamin industry, technical formulation innovations, global compliance protocols, and future B2B procurement trends.
When selecting a contract manufacturing partner for bulk vitamins, technical capabilities must be audited across three fundamental dimensions: delivery format versatility, particle engineering, and analytical verification testing.
Consumer preferences have decisively pivoted away from hard-pressed, difficult-to-swallow tablets toward experiential, highly bioavailable formats. Leading Chinese factories have invested millions in specialized production machinery:
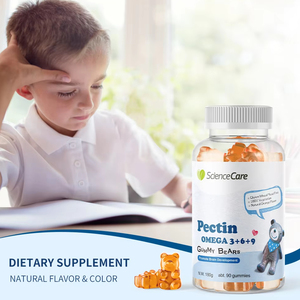
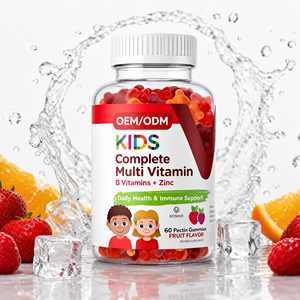
Unlike traditional animal-derived gelatin gummies that melt in warm transit climates and trigger religious dietary restrictions, modern clean-label manufacturing utilizes citrus and apple pectin matrices. Pectin requires high-precision cooking temperatures (105°C–110°C) and exact Brix/pH control to achieve optimal gelation, producing heat-stable, 100% vegan gummies suitable for global export.
Fat-soluble vitamins such as Retinol (Vitamin A), Vitamin D3, and Vitamin K2 MK-7 are prone to rapid oxidation when exposed to light, ambient humidity, or acidic gastric fluid. Advanced micro-encapsulation coats active lipid droplets in a protective carbohydrate or phospholipid shell, ensuring shelf-life stability up to 36 months and targeted intestinal absorption.
Equipped with modern automatic encapsulation machinery capable of outputting over 5.5 million capsules per day, facilities maintain nitrogen-purged blending hoppers. This eliminates dissolved oxygen during powder mixing, preserving sensitive active raw materials such as Menaquinone-4 (MK4) and Ascorbic Acid from degradation.
To eliminate risk of adulteration, heavy metal contamination, or potencies falling below label claims before shelf expiration, every single batch produced undergoes a strict multi-stage analytical workflow:
| Testing Stage | Methodology / Instrumentation | Parameters Verified | Compliance Threshold |
|---|---|---|---|
| Raw Material Receiving | FTIR Spectroscopy & HPLC | Raw Compound Identity & Purity | 100% Match to USP / EP Standard |
| In-Process Blending | Near-Infrared (NIR) Testing | Blend Homogeneity & Active Uniformity | RSD < 2.5% across batch |
| Contaminant Screening | ICP-MS (Inductively Coupled Plasma) | Heavy Metals (Lead, Arsenic, Cadmium, Mercury) | Prop 65 & FDA Action Levels |
| Microbiological Clearance | Rapid Automated Micro Systems | Total Plate Count, Yeast, Mold, E. coli, Salmonella | Absence of Pathogens; TPC < 1000 CFU/g |
| Finished Product CoA | HPLC / LC-MS/MS Assay | Label Claim Potency & Stability Overage | 100% - 115% of Stated Active Dose |
Strategic purchasing managers and brand directors must align their supply chains with evolving global regulatory frameworks and shift towards consumer-centric innovation. Over the next five years, four macro-trends will dominate global vitamin procurement:
Single-entity vitamin supplements (e.g., Vitamin D3 alone) are experiencing market saturation and declining retail price points. High-margin growth has migrated toward scientifically backed synergistic combinations. For instance, combining Vitamin K2 (MK-7 or MK-4) with Vitamin D3 directs calcium deposition into bone collagen matrices while preventing arterial calcification. Procurement contracts are shifting toward factories capable of micro-dosing K2 (measured in micrograms) homogeneously alongside macro-ingredients without potency loss.
E-commerce platforms like Amazon, alongside brick-and-mortar giants such as Target, CVS, and Walmart, have established stringent Certificate of Analysis (CoA) submission protocols. Importers can no longer rely on unverified factory-issued CoAs. Leading manufacturers now provide **ISO 17025 accredited third-party lab testing**, Certificate of Free Sale (CFS), Halal certification, Kosher documentation, and full cGMP batch production records (BPR) with every pallet exported.
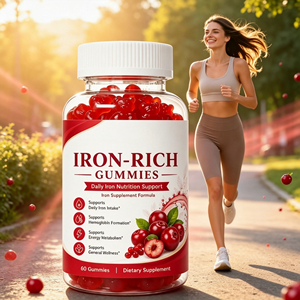
Nutraceutical consumers demand exceptional taste profiles without artificial colors or high-fructose corn syrup. Formulating iron-rich gummies or multivitamin protein powders presents complex challenges regarding metallic taste notes and vitamin B odor. Advanced Chinese contract manufacturers now employ natural masking technology using stevia, monk fruit, and organic botanical terpenes to deliver highly palatable adult and pediatric gummies.
To reduce inventory holding costs and test new SKU demand dynamically, emerging wellness brands require low Minimum Order Quantities (MOQs)—typically starting at 300 to 1,000 bottles for market-ready private label stock—coupled with rapid scale capacity (up to 100,000+ bottles per run) once retail traction is established. Modern automated facilities are built with flexible modular fill-lines to service both pilot launches and enterprise-level scale seamlessly.
Our manufacturing infrastructure represents the synthesis of international quality standards and robust Chinese industrial scalability. By integrating turnkey private label manufacturing, custom formulation R&D, and complete packaging automation under one NSF cGMP certified roof, we streamline the journey from product concept to retail shelf.
Our in-house team of formulation scientists, food technologists, and biochemists assist clients in engineering proprietary vitamin premixes, selecting stable bioactive salts, optimizing particle mesh sizes, and mastering flavor chemistry.
From HDPE bottles with child-resistant closures (CRC) for iron supplements to premium amber glass jars, induction heat sealing, pressure-sensitive tamper-evident neck bands, and blister packs—every container is engineered to prevent moisture ingress and preserve potency.
Avoid costly customs delays or regulatory warnings. Our compliance officers review Supplement Facts panels, active ingredient claims, allergen disclosure statements, and mandatory warnings to ensure compliance with regional target market laws.
Below are authoritative responses to the primary technical, operational, and regulatory queries encountered during international procurement audits:
Partner with a premier Chinese bulk vitamin manufacturer. Request technical specifications, request custom formulation samples, or get a direct factory quotation today.