Explore our export-ready, NSF 455-2 GMP certified product lineup engineered for optimal shelf stability, precision dosing, and retail packaging compliance.
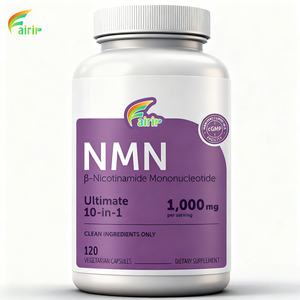
In the high-stakes global nutraceutical market, packaging is far more than a physical enclosure; it is the primary vector for product integrity, brand valuation, and regulatory compliance. As a premier Custom OEM Bottle Packaging Supplier & Exporter operating out of our state-of-the-art FDA-registered facility in Utah, USA, we integrate high-speed capsule encapsulation, powder blending, automated bottling, and high-barrier packaging under a unified NSF/ANSI 455-2 GMP quality framework. Fragmented supply chains introduce unacceptable risks of moisture degradation, microbial cross-contamination, and labeling delays. By engineering your supplement bottles, closures, induction seals, and outer secondary packaging within a single controlled environment, we ensure that every unit exiting our facility meets stringent physical, chemical, and microbiological parameters.
Our packaging infrastructure is designed specifically to solve the stability challenges inherent to sensitive bioactive compounds like 99% Pure Beta-Nicotinamide Mononucleotide (NMN), NAD+ boosters, enzyme complexes, and hydro-hygroscopic botanical powders. Unprotected exposure to humidity, oxygen, and atmospheric thermal spikes causes active ingredients to degrade, alter color, and lose potency. To combat this, our contract packaging lines feature automated nitrogen flushing, precision-placed silica desiccant canisters, and high-frequency induction foil sealing. This multi-layered barrier engineering guarantees minimal Moisture Vapor Transmission Rates (MVTR) and zero Oxygen Transmission Rates (OTR), ensuring your products maintain full label-claimed potency across international transit routes and multi-year retail shelf lives.
Full customization across Pharmaceutical-Grade Amber Glass, High-Density Polyethylene (HDPE), Polypropylene (PP), and Recycled PET (PCR) engineered to block harmful UV spectra.
In-line electromagnetic induction foil seamers create tamper-evident, leak-proof, and oxygen-impermeable hermetic seals across all bottle neck finishes.
Full-color pressure-sensitive labeling, shrink sleeve application, and regulatory Supplement Facts audit services conducted concurrently during filling.
Institutional supplement procurement is undergoing a paradigm shift driven by evolving environmental mandates, stringent cross-border eCommerce requirements, and consumer demand for anti-counterfeiting verification. Buyers across North America, Europe, Australia, and Asia are transitioning away from standardized, off-the-shelf packaging toward specialized, brand-owned OEM packaging molds and protective delivery architectures. Understanding these emerging macro trends is critical for procurement executives and brand directors looking to build resilient supply chains and maintain competitive margins.
1. Shift Toward Active Barrier Systems for Anti-Aging & Bioactive Compounds: The rapid commercial growth of cellular longevity actives, such as Beta NMN, CoQ10, and probiotics, has exposed the limitations of traditional packaging. Procurement strategies are now prioritizing active barrier systems that incorporate molecular-sieve desiccant caps and oxygen-scavenging resin additives directly into the bottle walls. These systems actively remove residual moisture trapped during the packaging cycle, preventing hydrolysis and oxidative degradation of active raw materials.
2. Sustainable Material Mandates & Post-Consumer Recycled (PCR) Polymers: Global environmental regulations, including EU packaging waste directives, are mandating higher percentages of PCR materials in retail bottles. Leading OEM exporters are now deploying food-contact approved 30% to 100% rHDPE and rPET containers that maintain mechanical durability and barrier performance while drastically reducing carbon footprints. Brands using sustainable, light-weighted bottles gain significant advantages in consumer preference and international customs clearance.
3. E-Commerce & Cross-Border Drop-Test Resilience: With direct-to-consumer (D2C) online subscriptions and Amazon FBA sales driving volume, bottle packaging must withstand harsh parcel transit dynamics. Legacy glass containers without specialized outer protective design suffer high breakage rates. Procurement leads are favoring custom impact-resistant HDPE packers, wide-mouth canisters, and specialized cap neck finishes (such as 38-400 and 45-400 continuous thread with child-resistant CR push-and-turn safety mechanisms) that pass ISTA-6A drop-test criteria without liquid or powder leakage.
4. Smart Packaging & Anti-Counterfeiting Integration: Counterfeit dietary supplements pose severe financial and reputational hazards in global export channels. Modern OEM bottle packaging incorporates unit-level QR coding, invisible UV inks, and tamper-evident shrink bands with embedded holographic security threads. These features enable consumers and customs officials to instantly verify product authenticity and trace batch genealogy back to the manufacturing plant.
Selecting the optimal container material and closure system requires evaluating chemical compatibility, moisture sensitivity, light barrier needs, and freight parameters. The matrix below outlines our engineering specifications for export-grade bottle manufacturing:
| Packaging Material | Barrier Efficiency (UV / MVTR) | Impact Resistance | Ideal Application | Export Freight Profile |
|---|---|---|---|---|
| Amber HDPE Packer | Excellent (UV) / High (MVTR) | Superior (Unbreakable) | NMN Powder, Capsules, Hygroscopic Botanicals | Lightweight, Reduced Express Shipping Costs |
| Amber Pharmaceutical Glass | Maximum (UV) / Impermeable | Moderate (Requires Cushioning) | Premium Oil Softgels, Specialty Liquids, Tinctures | Heavy Weight, High-End Retail Positioning |
| Post-Consumer Recycled PET | Good (UV with tint) / Medium | High (Flex-Resistant) | Daily Multivitamins, Sports Nutrition Powders | Eco-Compliant, Cost-Effective International Freight |
| Aluminum Canisters & Tins | 100% Light & Air Impermeable | Very High (Dent Resistant) | Effervescent Tablets, Pre-Workout Powders | Premium Modern Aesthetic, Fully Recyclable |
As the global health and wellness sector expands toward a projected market value exceeding $300 billion by 2030, contract packaging suppliers must continuously innovate. The intersection of pharmaceutical chemistry, material science, and automated manufacturing is redefining how supplements are preserved and delivered to end consumers.
One major developmental trajectory is the integration of smart dosing technology directly within bottle closures. Innovative cap designs now feature built-in compartment dividers, moisture indicator rings that shift color when internal humidity thresholds are breached, and digital Bluetooth-enabled reminders for medical-grade compliance. For high-value bioactive ingredients like pure NMN powder (CAS 1094-61-7), these packaging advancements ensure that degradation is flagged long before the product reaches the consumer's hands.
Furthermore, automated vision-inspection systems installed across our Utah bottling lines represent the gold standard in quality control. Every bottle passing down our filling lines undergoes high-speed optical scanning to verify:
1. Precise fill heights and capsule counts via photoelectric sensors.
2. 100% induction seal continuity without microscopic pinholes or heat scorches.
3. Flawless label alignment, batch code legibility, and expiration date printing.
4. Correct cap torque application to prevent vibrational loosening during ocean container or air freight transit.
This relentless focus on automation eliminates human error, minimizes batch rejections, and ensures that overseas importers receive pristine, market-ready finished goods that strictly comply with FDA 21 CFR Part 111 regulations and international health authority standards.
Navigating international custom manufacturing requires a production partner with verified credentials, institutional scale, and deep regulatory expertise. As a leading US-based contract manufacturer and contract packaging exporter, Vox Nutrition offers unique operational advantages that insulate your brand from market volatility:
Our Utah facility undergoes independent, rigorous third-party audits to guarantee absolute adherence to strict Good Manufacturing Practices (GMP) for dietary supplements.
We perform graphic layout reviews, Supplement Facts panel compliance checks, high-definition flexographic printing, and bottle application under one roof.
We furnish complete export dossiers, including Certificates of Analysis (CoA), Certificates of Free Sale, BSE/TSE-Free Statements, and Allergen Declarations for global customs clearance.
Here are detailed answers to key technical and operational questions frequently raised by brand owners, importers, and procurement directors:
For market-ready private label formulations in standard bottle configurations, MOQs start at very accessible low unit counts (typically 300 to 1,000 bottles per SKU). For custom contract formulations requiring bespoke raw material blending, specific capsule colors, or unique bottle molds, MOQs generally start around 3,000 to 5,000 bottles depending on raw material blend parameters.
Sensitive actives like 99% Beta NMN and NAD+ precursors are packaged using high-density amber HDPE or UV-coated glass containers paired with pharmaceutical-grade silica desiccant packs and thick induction foil liners. Furthermore, we offer climate-controlled export palletizing and refrigerated container shipping (Reefer transport) for international routes passing through high-humidity tropical zones.
Yes. We offer complete custom tooling and cosmetic design options. Brands can select from amber, white, clear, cobalt blue, or custom pantone-matched bottle colors, along with specialized closures including ribbed continuous-thread caps, child-resistant safety caps, metal screw tops, and custom-printed tamper-evident neck bands.
Every single batch produced and packaged in our facility is issued a comprehensive Certificate of Analysis (CoA). This document verifies HPLC ingredient potency assays, heavy metal limits (Lead, Arsenic, Cadmium, Mercury via ICP-MS), microbial pathogen screens (E. coli, Salmonella, Yeast & Mold), and physical bottle seal integrity checks.
Standard turnaround time for existing catalog formulations with client-approved artwork is typically 2 to 4 weeks. Custom formulation blending, encapsulation, stability testing, and automated bottling cycles typically range from 6 to 8 weeks depending on raw material sourcing leads and custom printing schedules.
Absolutley. We configure all primary bottle containers, master cartons, and pallet configurations to meet or exceed Amazon FBA packaging guidelines, barcode scannability requirements, and major retail chain (Walmart, Target, CVS) intake specifications, including suffocation warnings and tamper-evident seals.
Ready to launch or scale your dietary supplement line with high-capacity encapsulation, precision bottling, and certified export compliance? Contact our technical engineering team today for custom quotes, material samples, and formulation assistance.
Contact Us