Direct factory supply of pharmaceutical-grade Beta-Nicotinamide Mononucleotide (CAS 1094-61-7). Available in bulk raw powder, customized vegetable capsules, and fully packaged retail bottles.
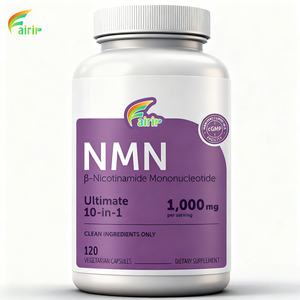
A comprehensive guide for procurement directors, brand owners, and scientific officers on scaling high-potency Beta-Nicotinamide Mononucleotide (NMN) products with full cGMP compliance.
Unlike standard chemical synthesis that leaves hazardous solvent residues or heavy metal contaminants, our fully enzymatic bio-catalytic process yields 99.0%+ pure Beta-NMN (CAS 1094-61-7) matching biological molecular structures for maximal cellular uptake and NAD+ conversion.
We provide full-spectrum contract manufacturing options including enteric-coated capsules (preventing gastric degradation), sublingual fast-melt powders, liposomal liquid-filled capsules, and synergistic longevity stacks combined with Trans-Resveratrol, PQQ, and CoQ10.
Every single raw batch undergoes stringent third-party independent laboratory testing. Analytical testing protocols include High-Performance Liquid Chromatography (HPLC) for assay purity, ICP-MS for heavy metals (Pb, As, Cd, Hg), and microbial limits according to USP <2021/2022>.
Selecting the optimal synthesis pathway is crucial for brand positioning, regulatory submission, and end-user bio-efficacy. Below is an analytical matrix comparing NMN manufacturing technologies:
| Evaluation Parameter | Enzymatic Synthesis (Our Standard) | Chemical Synthesis | Microbial Fermentation |
|---|---|---|---|
| Purity Level (HPLC) | ≥ 99.0% to 99.8% Pure Beta-Isomer | 95.0% - 98.0% (Contains Alpha-Isomers) | 85.0% - 92.0% (Requires Heavy Extraction) |
| Biological Stereospecificity | 100% Bio-identical Beta-NMN | Mixed stereoisomers (Lower Activity) | Natural Beta-Form |
| Residual Solvents & Impurities | Zero Toxic Solvents (Water-based Process) | Potential Chemical Traces (Requires Removal) | High Protein & Endotoxin Residue Risk |
| Bulk Stability & Bulk Density | High Density (0.45 - 0.65 g/mL), Heat Stable | Variable Bulk Density, Moisture Sensitive | Hygroscopic, Rapid Color Degradation |
| Production Scalability & Cost | Optimal Cost-to-Purity Ratio for Scale | Low Initial Cost / High Regulatory Risk | High Cost / Limited Large-Scale Yield |
Our Utah-based manufacturing infrastructure operates under strict FDA registration and NSF/ANSI 455-2 cGMP certification for dietary supplements. We eliminate multi-vendor friction by housing raw material sourcing, automated blending, high-speed encapsulation, in-house label printing, bottling, and fulfillment under one single compliance-driven roof.
"Contract manufacturing is not just about compounding powder into capsules; it is about building bulletproof analytical documentation that stands up to global regulatory intake and consumer scrutiny."
FTIR identity testing, HPLC purity verification, heavy metals, and microbiological screening prior to batch release.
High-capacity V-blenders ensuring homogenous active ingredient dispersion across multi-ingredient complex longevity formulations.
Weight-monitored high-speed filling, heat-induction inner sealing, tamper-evident neck shrink banding, and blister packing.
Final CoA issuance, stability sample retention, Master Manufacturing Batch Records (MMR) archiving, and direct freight dispatch.
How global buyer intent, emerging regulatory frameworks, and advanced delivery technologies are reshaping the nutraceutical supply chain over the next decade.
Procurement intent is shifting rapidly from standard unformulated NMN powders to advanced liposomal encapsulation and sublingual delivery formats. Liposomal phospholipids shield Beta-NMN from enzymatic breakdown in the digestive tract, increasing cellular absorption by up to 4.5x compared to standard raw capsules.
Monotherapy SKUs are giving way to integrated cellular health formulas. Procurement teams are requesting custom contract blends combining NMN with NAD+ boosters (NR, Nicotinamide), Sirtuin activators (Pterostilbene, Trans-Resveratrol), mitochondrial support agents (CoQ10, PQQ), and cognitive enhancers (Creatine Brainberry®).
Institutional buyers and major marketplace platforms now demand full transparent supply chain validation. Future procurement requires lot-specific QR codes printed on consumer bottles leading directly to third-party independent lab Certificates of Analysis (CoA) verifying assay potency and zero heavy metal contamination.
Sustainability is no longer optional in global procurement RFQs. Buyers prioritize OEM manufacturers utilizing zero-solvent enzymatic biosynthesis that reduces carbon footprints by 60%, combined with biodegradable pouches, PCR (Post-Consumer Recycled) plastic bottles, and glass packaging alternatives.
With global regulatory bodies increasing scrutiny over anti-aging claims and ingredient identity, brand longevity hinges on manufacturing inside FDA-registered, NSF/ANSI 455-2 cGMP certified plants that ensure compliance with 21 CFR Part 111 dietary supplement guidelines.
To reduce capital risk during new product launches, modern brands are seeking OEM contract manufacturers offering flexible scaled MOQs—starting with 300 to 1,000 bottles for market testing before expanding into 50,000+ unit high-speed automated runs.
From micro-encapsulation to continuous enzymatic catalysis, discover how modern manufacturing science is optimizing ingredient bioavailability and shelf stability.
The global dietary supplement contract manufacturing sector is undergoing a profound paradigm shift driven by biological analytics, cellular delivery engineering, and automated quality control. As consumer literacy around cellular metabolic pathways (such as NAD+ synthesis, mitochondrial biogenesis, and sirtuin activation) increases, product developers can no longer rely on simple powder blends.
Enzymatic Immobilization Technology: Modern OEM facilities are deploying fixed-bed enzymatic reactors where immobilized bio-enzymes continuously convert nicotinamide derivatives into high-purity Beta-NMN. This continuous flow processing dramatically reduces batch-to-batch variance, guarantees zero chemical cross-contamination, and achieves HPLC purity levels consistently exceeding 99.5%.
Targeted Gastric Bypass & Enteric Protection: One of the primary engineering hurdles in oral NMN delivery is avoiding degradation by stomach acid. Innovations in acid-resistant hydroxypropyl methylcellulose (HPMC) polymer shells allow capsules to pass intact through the stomach environment and release active Beta-NMN directly into the intestinal tract, where dedicated SLC12A8 transporters facilitate direct cellular entry.
AI-Powered Granulation & Particle Size Optimization: Advanced jet-milling and laser diffraction particle size analysis allow contract manufacturers to control NMN bulk density and micronization (typically targeting 80–120 mesh size). Micro-fine uniform particle distribution prevents capsule weight variation on automated filling machines, enabling encapsulation speeds of up to 120,000 units per hour without sacrificing weight precision.
Answers to common operational, regulatory, and logistics queries submitted by global procurement teams and brand owners.
For market-ready private label formulas using our standard stock capsule and bottle options, MOQs start as low as 300 to 500 bottles per SKU. For custom contract formulations requiring bespoke ingredient blending, unique capsule sizes, or custom powder formulations, MOQs typically start at 1,000 units for powders and 5,000 units for custom capsules.
Every completed batch is released with a comprehensive Certificate of Analysis (CoA). Testing documentation includes High-Performance Liquid Chromatography (HPLC) assay purity testing (verifying ≥99.0% Beta-NMN content), Heavy Metal ICP-MS screening (Lead, Arsenic, Cadmium, Mercury), USP <2021/2022> Microbiological testing, and physical inspection records.
For standard private label repeat orders with existing artwork on file, lead times are typically 2 to 3 weeks. New custom formulation projects involving R&D formulation, pilot bench sampling, raw material sourcing, stability testing, and label compliance review generally take 4 to 6 weeks from final sign-off.
All products are manufactured in our FDA-registered facility located in Utah, USA, certified to NSF/ANSI 455-2 cGMP standards for dietary supplements. The facility maintains organic certification via the Utah Department of Agriculture and Food (UDAF) and is an active member of the Natural Products Association (NPA).
Yes. Our in-house regulatory compliance team reviews all artwork, Supplement Facts panels, allergen declarations, structure/function claim language, and barcode placements to ensure full adherence to FDA 21 CFR Part 101 labeling requirements before printing.
Enzymatic synthesis uses natural biological enzymes to produce 100% pure Beta-Nicotinamide Mononucleotide identical to the NMN produced naturally inside the human body. Chemical synthesis often leaves residual organic solvents and produces inactive alpha-isomers that reduce biological effectiveness.
Absolutley. We handle all marketplace intake preparation including lot and expiration inkjet coding, tamper-evident neck shrink banding, master carton box barcoding, inner-pack bundling, and direct palletized freight delivery to Amazon fulfillment centers or retail distribution hubs.
For custom contract manufacturing projects where our R&D team develops a unique proprietary blend specifically for your brand, your enterprise retains full ownership of the finished formulation specifications upon project completion.
Partner with an NSF/ANSI 455-2 cGMP certified US manufacturer. Request factory-direct pricing, custom formulation quotes, and bulk raw material sample kits today.
Send an Inquiry