In the rapidly evolving landscape of global nutraceuticals, consumer demand has shifted decisively from crude botanical powders to bio-engineered, highly standardized plant extracts and cellular longevity compounds such as Beta-Nicotinamide Mononucleotide (Beta-NMN, CAS 1094-61-7). As a premier US-based private label supplement manufacturer operating an NSF/ANSI 455-2 cGMP certified and FDA-registered facility in Utah, our plant infrastructure sets the benchmark for contract manufacturing excellence.
Achieving commercial viability and therapeutic efficacy in custom OEM herbal extract manufacturing requires a granular understanding of molecular stability, enzymatic biocatalysis, structural identification, and bioavailability optimization. Traditional solvent-extraction methods often suffer from thermal degradation, solvent residues, and batch-to-batch active marker variability. To address these industry-wide bottlenecks, our specialized extraction and enzymatic synthesis platforms leverage state-of-the-art closed-loop technologies.
A core differentiator in our longevity ingredient manufacturing pipeline is the transition from chemical synthesis to direct enzymatic biocatalysis for Beta-Nicotinamide Mononucleotide production. Chemical synthesis routes often yield residual chemical solvents, heavy metal traces, and toxic alpha-isomer contaminants that diminish cellular uptake and jeopardize regulatory intake approval.
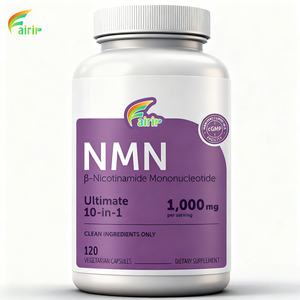
Our fully enzymatic process mimics biological NAD+ biosynthesis by utilizing specific ATP-dependent nicotinamide phosphoribosyltransferase (NAMPT) biocatalysts. This yields a biologically active β-anomer with purity consistently exceeding 99.0% by HPLC, featuring zero trace chemical residues and negligible α-isomer impurity (<0.1%).
| Analytical Parameter | Industry Standard Requirement | Our OEM Factory Specification | Testing Methodology |
|---|---|---|---|
| Chemical Identification | Positive Reference Standard Match | 100% Conforms to Molecular Structure | FTIR / 1H-NMR Spectroscopy |
| HPLC Assay Purity | ≥ 98.0% Total Anomers | ≥ 99.0% Pure β-Nicotinamide Mononucleotide | High-Performance Liquid Chromatography |
| Heavy Metals (Pb, Cd, Hg, As) | < 10.0 ppm Total | < 1.0 ppm Combined Trace Limits | ICP-MS (Inductively Coupled Plasma) |
| Residual Organic Solvents | Meet USP <467> Limits | Zero Residual Class 1 & Class 2 Solvents | Headspace GC-MS |
| Microbial Bioburden | TPC < 10,000 CFU/g | TPC < 1,000 CFU/g; Zero Pathogens | USP <61/62> Microbiological Panel |
| Bulk Density & Flowability | 0.30 – 0.50 g/mL | Optimized 0.45 – 0.65 g/mL (High Density) | Tap Density Tester / Carr's Index |
Raw botanical extracts and crystalline NMN powders often display poor aqueous solubility and rapid gastrointestinal degradation. As part of our comprehensive OEM contract services, our formulation lab integrates micronization, fluid-bed granulation, and liposomal encapsulation. By controlling particle size distribution ($D_{90} < 15 \mu m$) through specialized jet milling, we dramatically increase surface area contact, accelerating intestinal dissolution rates and enhancing cellular permeability via Slc12a8 transporters.
Brand owners and B2B buyers evaluating private label manufacturing partners must align with multi-year macro shifts in global health and regulatory policy. Based on analytical data from global marketplace intake requirements, four key trends define the future of botanical extract contract manufacturing:
Regulatory bodies are moving beyond basic UV-Vis spectrophotometry toward DNA barcoding and HPLC fingerprinting to eradicate adulteration, species substitution, and synthetic filler inflation in raw botanical stocks.
Supercritical $CO_2$ extraction and aqueous enzymatic processes are replacing toxic organic solvents (hexane, methanol). Brands specifying solvent-free extraction gain significant clean-label market leverage.
Single-ingredient SKUs are giving way to advanced synergistic matrices. Combining Beta-NMN with polyphenols (Resveratrol, Pterostilbene, Quercetin) optimizes NAD+ metabolic salvage pathways via SIRT1 enzyme activation.
Building a global supplement brand requires an OEM manufacturing partner that eliminates supply chain friction, mitigates regulatory risks, and executes continuous high-volume production without sacrificing quality control. Our US facility bridges the gap between raw botanical synthesis and retail-ready finished packaging.
Equipped with high-speed automated encapsulation machinery capable of delivering over 5.5 million capsules daily across vegetable (HPMC), pullulan, and gelatin shells. Our powder blending operations utilize 3D V-blenders for absolute homogeneity.
Certified to the gold-standard NSF/ANSI 455-2 dietary supplement GMP standards and fully registered with the US FDA. Every production lot includes full master batch records, certificates of analysis (CoAs), and end-to-end material traceability.
Consolidate your supply chain under one roof. We manage container sizing, high-speed bottling, induction heat sealing, tamper-evident neck banding, and full-color in-house label printing to accelerate time-to-market.
Products manufactured in our facility successfully navigate strict intake audits for Amazon FBA, club stores, specialty pharmacy chains, and big-box retailers. We handle Amazon-compliant lab testing documentation and barcode/pallet setup.
Skip months of preliminary formulation research and development. Choose from over 115 stability-tested, pre-formulated turnkey stock products spanning longevity, sports nutrition, joint health, cognitive enhancement, and digestive wellness.
For our market-ready stock private label formulas (such as standard Beta-NMN capsules or standardized botanical single-ingredient SKUs), MOQs start at low unit thresholds—typically a few hundred bottles per order. This low barrier allows growing brands to validate market traction quickly. For completely custom contract formulations involving bespoke extract blending, specialized particle micronization, or proprietary flavoring systems, MOQs generally start at 1,000 units for powders and 5,000 units for encapsulated SKUs due to raw material equipment setup requirements.
Every batch of incoming raw material undergoes strict quarantine upon entering our Utah manufacturing facility. Sampling is conducted according to ANSI/ASQ Z1.4 inspection standards. Identity is confirmed using High-Performance Liquid Chromatography (HPLC), Fourier-Transform Infrared Spectroscopy (FTIR), or Thin-Layer Chromatography (TLC). Chemical purity, heavy metals (ICP-MS), residual solvents (Headspace GC-MS), pesticide residues, and microbiological bioburdens are rigorously tested before raw ingredients are cleared for blending.
Re-orders for existing private label products with pre-approved artwork typically ship within 2 to 3 weeks. Initial custom formulation projects require 6 to 8 weeks to allow for complete R&D pilot batching, pilot stability evaluation, ingredient sourcing, compliance review of Supplement Facts panels, and custom label printing. We publish clear, milestone-driven project schedules so brand owners can coordinate launch marketing with absolute precision.
Yes. Products manufactured in our facility meet all current compliance requirements for sales on Amazon, including ISO/IEC 17025 accredited laboratory CoA documentation, Certificate of Analysis for active dietary ingredients, and strict adherence to FDA 21 CFR Part 111 cGMP regulations. For international buyers, we provide Certificates of Free Sale (CFS), BSE/TSE-free declarations, and detailed ingredient dossier breakdowns required by regional health authorities across Europe, Asia-Pacific, and the Middle East.
When you engage our team for custom contract manufacturing, the proprietary formula developed specifically for your brand remains 100% your intellectual property. We execute comprehensive Non-Disclosure Agreements (NDAs) prior to initial technical discussions. Conversely, stock private label formulas utilize our proven in-house IP, allowing you to market established formulas immediately under your brand identity.
Absolutely. Operating a multi-department 5.5M/day capsule encapsulation line alongside high-capacity powder filling suites allows us to execute cross-category product lines simultaneously. Brands often launch matching product ecosystems—such as NMN Longevity Capsules alongside an Electrolyte Powder Blend—under one dedicated project manager, one unified compliance audit, and consolidated logistics shipping.
Partner with an NSF GMP-certified US manufacturer. Access 115+ market-ready formulas, custom biocatalytic synthesis, and high-speed contract packaging today.