OEM/ODM Supplement Softgels Manufacturers & Exporter

Global Contract Manufacturing & Private Label Whitepaper: Bioavailability Engineering, Advanced Encapsulation, and Turnkey Sourcing Solutions

High-Demand Softgel & Bulk Supplement Offerings

Market-tested, high-purity active ingredients ready for private label packaging, custom softgel matrix encapsulation, and global export.
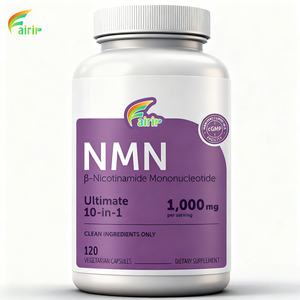
OEM Private Label 99% Beta NMN Capsules and Softgels

OEM Private Label 99% Beta Nicotinamide Mononucleotide (NMN) Capsules & Softgel Complex

Send an Inquiry
Bulk High Quality NMN Powder CAS 1094-61-7

Pharmaceutical Grade Bulk NMN Powder CAS 1094-61-7 99% Pure Raw Material

Send an Inquiry
NMN Supplements Cosmetic and Food Grade Powder

Custom OEM NMN Cellular Longevity Formula (Cosmetic & Food Grade Standard)

Send an Inquiry
Bulk Sale Beta-Nicotinamide Mononucleotide Pure Powder

Bulk Contract Supply Pure Beta-Nicotinamide Mononucleotide (In-Stock Fast Shipping)

Send an Inquiry
Fast Delivery NMN 99% Micro-encapsulated Raw Material

Ultra-Pure High Bioavailability 99% NMN Lipid Blend Raw Material

Send an Inquiry
Wholesale Bulk NMN 99% Pure Private Label Solution

Wholesale Private Label NMN Anti-Aging Softgel & Capsule Formulations

Send an Inquiry
High Quality Food Grade NMN Powder Pure Material

High-Grade Food & Dietary Supplement Beta-Nicotinamide Mononucleotide Complex

Send an Inquiry
CHTNature Bulk Beta Nicotinamide Mononucleotide Powder

Standardized Export Grade Beta NMN CAS 1094-61-7 (Custom Softgel Ready)

Send an Inquiry
5.5M+
Daily Encapsulation Unit Output
NSF/ANSI
455-2 GMP Certified Facility
115+
Market-Ready Standard Formulas
28+
Years Manufacturing Expertise

State-of-the-Art Utah Facility & Quality System Infrastructure

Delivering uncompromised batch-to-batch consistency, compliance security, and bio-enhanced oil encapsulation under one certified roof.

NSF/ANSI 455-2 & FDA cGMP Certified

Our US-based facility operates in strict adherence to cGMP protocols. Every production line undergo independent third-party audits by NSF International, guaranteeing that your brand meets stringent dietary supplement regulations globally.

Advanced Rotary Die Softgel Machinery

Equipped with automated continuous gelatin melting systems, precision fill pumps, and humidity-controlled drying tunnels, our plant handles lipid solutions, hydrophobic suspensions, and micro-emulsions with exact dosage uniformity.

In-House Analytical Quality Assurance

Raw materials undergo mandatory quarantine and chemical verification via HPLC, GC-MS, and ICP-MS for heavy metals, pesticides, and solvent residue. Every finished lot comes backed by a comprehensive Certificate of Analysis (CoA).

Turnkey Private Label & Bottling

Eliminate multi-vendor friction. We provide end-to-end packaging services: custom bottle sizing, PET/HDPE resin options, induction sealing, tamper-evident shrink bands, and compliant Supplement Facts panel printing on-site.

Strict Allergen & Cleanroom Segregation

Our Utah manufacturing suites strictly enforce cross-contamination controls for soy, fish oil, gelatin, and botanical extract processing. USDA Organic certified handling through UDAF ensures clean label integrity.

Global Regulatory Export Compliance

We export to over 40 countries across North America, Europe, Asia-Pacific, and the Middle East. Our regulatory affairs team assists with customs clearance documentation, Certificate of Free Sale (CFS), and market intake rules.

Softgel Technology: Bioavailability Engineering & Matrix Formulation Science

In the competitive dietary supplement sector, softgel encapsulation represents the premier delivery technology for lipophilic, poorly water-soluble, and oxidation-sensitive active ingredients. Compared to traditional hard-shell capsules and compressed tablets, softgels deliver superior metabolic absorption, uniform dose precision, and robust barrier protection against ambient oxygen and moisture degradation.

1. Fill Formulation Categories: Solution, Suspension, and Emulsion Systems

The internal matrix of a softgel capsule can be engineered across three distinct physical states based on the physicochemical properties of the active pharmaceutical ingredients (APIs) or nutraceutical compounds:

  • Lipophilic Solutions: Actives such as Omega-3 (EPA/DHA), CoQ10, Vitamin D3/K2, Astaxanthin, and Curcumin are solubilized directly into lipid carriers (e.g., Medium-Chain Triglyceride (MCT) oil, extra virgin olive oil, or sunflower lecithin). This eliminates rate-limiting dissolution steps in the gastrointestinal tract.
  • Hydrophobic Suspensions: High-dose botanical extracts or crystalline powders (such as NMN, Resveratrol, or Calcium complexes) are milled into micronized particles (< 180 microns) and suspended in a structured oil-wax vehicle to prevent phase separation during encapsulation.
  • Self-Emulsifying Drug Delivery Systems (SEDDS): Advanced surfactant-lipid combinations that spontaneously form micro-emulsions upon contact with gastric fluids, drastically expanding surface area and driving lymphatic absorption.

2. Shell Matrix Chemistry: Gelatin Bloom Strength vs. Plant-Based Polymers

The protective outer shell determines structural stability, disintegration timing, and target consumer appeal. OEM buyers can select from engineered shell options:

  • Pharmaceutical Bovine/Porcine Gelatin: Utilizing 150 to 200 Bloom strength gelatin combined with plasticizers (glycerin, sorbitol) to yield optimal ribbon elasticity, thermal resistance, and rapid gastric disintegration (< 15 minutes).
  • Vegan Tapioca & Seaweed Hydrocolloids: Derived from non-GMO tapioca starch and carrageenan. Offers higher thermal tolerance (up to 45°C without deformation), making plant-based softgels ideal for hot-climate export logistics.
  • Enteric-Coated & Targeted-Release Shells: Applied via specialized aqueous film coating or integrated polymeric shell modifiers. Protects acid-sensitive enzymes or probiotics from stomach acid, releasing contents intact within the alkaline pH of the small intestine.

Comparative Engineering Matrix: Softgel Formulations vs. Hard Capsules vs. Tablets

Technical Parameter Lipid Softgel Capsule Standard Two-Piece Capsule Compressed Tablet
Bioavailability Index (Lipids) Maximum (Direct Solubility) Moderate (Requires In-Vivo Dissolution) Low (Disintegration Friction)
Oxygen & Light Shielding Hermetically Sealed Shell Permeable Mechanical Seam Exposed Matrix Surface
Dose Uniformity Tolerance < ±1.5% Fill Weight Variation < ±3.5% Powder Fill Variation < ±5.0% Compression Variation
Consumer Swallowing Compliance Optimal (Smooth, Flexible Shell) Moderate (Friction Friction) Poor (Hard Edge Chalkiness)
Target Release Flexibility Gastric, Enteric, Dual-Release Gastric & Acid-Resistant Sustained-Release Matrix

Future Procurement & Market Development Trends in Softgel Manufacturing

Navigating evolving consumer expectations, regulatory tightening, and novel active ingredient delivery technologies for the next decade.

1. Surge in Plant-Based & Clean-Label Shell Demand

Global brand buyers are rapidly transitioning away from animal gelatin toward modified tapioca and pullulan matrices. Driven by halal, kosher, and vegan consumer segments, clean-label plant softgels now represent over 35% of new product developments in European and North American markets. Contract manufacturers with high-speed plant-softgel machinery hold a decisive supply chain advantage.

2. Cellular Longevity & NAD+ Precursor Oil Suspensions

The longevity nutrition market has shifted from basic single-ingredient powders to bio-enhanced lipid suspensions. Combining high-purity Beta-NMN, NAD+ boosters, Ergothioneine, and Urolithin A with liposomal sunflower lecithin in softgel formats prevents atmospheric oxidation and enhances lymphatic systemic uptake—creating high-margin hero SKUs for premium brands.

3. TOTOX Score Transparency & Lipid Oxidation Control

Retail chain buyers and regulatory authorities now demand full transparency on Total Oxidation (TOTOX) values for marine and algae oil softgels. Advanced OEM facilities utilize continuous nitrogen purging throughout receiving, blending, and encapsulation to maintain peroxide values (PV) below 5 meq/kg and anisidine values (AV) below 20, guaranteeing fresh, odor-free end products.

4. Supply Chain Consolidation & Turnkey CDMO Sourcing

Fragmented sourcing—where raw materials, encapsulation, and label printing are handled by separate vendors—is being replaced by single-site CDMO partnerships. Brands reduce lead times from 16 weeks to under 4 weeks by selecting manufacturers capable of handling raw material identity testing, custom encapsulation, in-house label printing, and automated bottling under one roof.

Comprehensive Analytical Testing & Release Protocols

Rigorous multi-stage quality control checks applied to every batch prior to commercial release and international shipment.

Phase I: Raw Material Verification

100% of incoming active ingredients, carrier oils, and shell polymers are quarantined. FTIR spectroscopy verifies chemical identity; HPLC assays determine exact potency; ICP-MS screens for heavy metals (Lead, Arsenic, Cadmium, Mercury) down to parts-per-billion (ppb) limits compliant with California Proposition 65.

Phase II: In-Process Micro-Monitoring

During the rotary die encapsulation run, automated sensors perform laser shell-thickness monitoring every 15 minutes. In-line weight checks ensure fill tolerances within ±1.0%. Seam integrity is evaluated via microscopic seam-width cross-sectioning to eliminate potential field leakage.

Phase III: Finished Good Certificate of Analysis

Finished softgels undergo USP <2040> rupture and disintegration testing, total aerobic microbial count (TAMC), yeast & mold enumeration, and pathogen screening (E. coli, Salmonella, S. aureus). Retention samples are archived in climate-controlled rooms for shelf-life stability verification.

Frequently Asked Questions (B2B Buyer Sourcing Guide)

Direct technical and commercial answers for brand managers, procurement directors, and global importers.

What are the minimum order quantities (MOQ) for custom OEM softgel manufacturing vs. private label?

Market-ready private label softgels using our established stock formulas start at low unit volumes, typically 300 to 500 bottles per SKU, allowing brand owners to rapidly validate market traction. Custom contract formulations require larger batch runs due to raw material prep, ribbon gel setup, and machine calibration—custom softgel runs typically start at 100,000 to 300,000 capsules depending on die shape, active complexity, and shell material selection.

What is the standard production timeline from purchase order to export shipment?

For existing private label formulas with pre-approved artwork, turn-around times range between 2 to 4 weeks. Custom contract manufacturing projects require approximately 6 to 8 weeks, which accounts for pilot blending, raw material verification, stability trial runs, softgel drying cycles, and analytical CoA testing prior to pallet release.

Can you encapsulate specialized active oils like NMN oil suspensions, CoQ10, and high-concentration EPA/DHA?

Yes. Our facility specializes in hydrophobic, heat-sensitive, and lipophilic active suspensions. We utilize inert nitrogen gas blanket protection during oil slurry preparation to prevent oxidation of delicate lipids, ensuring high potency retention over the product's full shelf life.

Which regulatory compliance documents are provided for international export customs clearance?

We provide a complete export documentation bundle including: batch-specific Certificate of Analysis (CoA), Certificate of Free Sale (CFS), cGMP Compliance Certificate (NSF/ANSI 455-2 standard), Allergen Declaration, Non-GMO Certificate, and complete Master Batch Records upon request.

What customization options exist for softgel shape, sizing, and shell coloring?

We offer an extensive selection of tooling dies: Oval (Sizes 3 to 20), Oblong (Sizes 4 to 22), Round (Sizes 3 to 40), and specialized twist-off shapes. Shells can be customized with clear, opaque, or two-tone colors using natural, clean-label colorants (such as chlorophyll, riboflavin, or caramel) with natural flavor masking (peppermint, citrus, vanilla).

How does your facility guarantee Amazon and major retail supply chain acceptance?

Products manufactured in our FDA-registered, NSF GMP facility are pre-vetted to meet Amazon Dietary Supplement Verification requirements, as well as intake standards for national retail pharmacy and club store chains. We oversee label artwork compliance, barcode scannability, lot coding, shrink banding, and carton stacking specifications to ensure zero intake rejections.

Ready to Scale Your Softgel & Supplement Brand?

Partner with a certified US manufacturer & exporter. Request a detailed factory quote, sample batch evaluation, or formulation consultation with our technical team today.