Directly sourced Himalayan raw mineral pitch processed under cGMP standards. Available in purified resin, standardized powder, encapsulated matrices, and ready-to-consume oral stick packs.
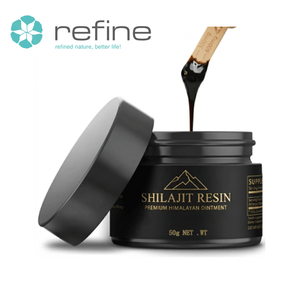
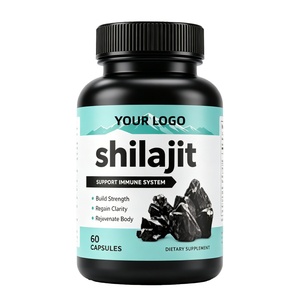
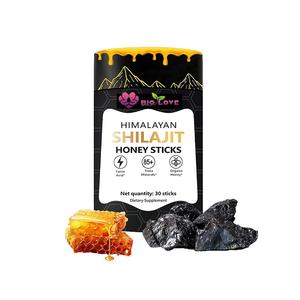
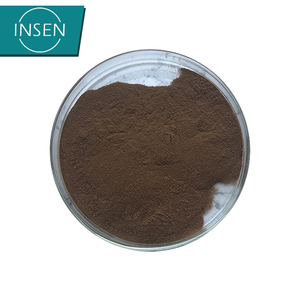
Why generic raw pitch fails modern regulatory intake and how pharmaceutical-grade water extraction delivers stable bio-available fulvic complexes.
Traditional suppliers often quote 50% or 60% fulvic acid based on outdated gravimetric (calcium precipitation) methods, which false-positive for humic impurities and lignins. Our manufacturing process utilizes High-Performance Liquid Chromatography (HPLC) and ISO-certified spectrophotometry to verify genuine low-molecular-weight fulvic complexes, ensuring reproducible biological activity from batch to batch.
The true therapeutic engine of premium Shilajit lies in its carrier molecules: dibenzo-α-pyrones (DBPs) and conjugated chromoproteins. These compounds act as mitochondrial electron transporters, facilitating ATP generation. Our proprietary low-temperature aqueous refinement preserves delicate DBP complexes that thermal scorching typically destroys.
Raw rock resin inherently contains geological heavy metal deposits including lead, arsenic, cadmium, and mercury. We employ multi-stage centrifugal filtration paired with counter-current resin technology. Every lot undergoes Inductively Coupled Plasma Mass Spectrometry (ICP-MS) validation to guarantee levels far below strict California Prop 65 and EU directives.
Comparative parameter guide for procurement officers, quality control assurance managers, and product development engineers.
| Specification Parameter | Raw Rock Resin (Unrefined) | Standardized Water-Soluble Powder | Ultra-Pure Bio-Active Extract (HPLC) |
|---|---|---|---|
| Fulvic Acid Content | 10% – 25% (Variable) | 40% – 50% (Standardized) | 50% – 65%+ (HPLC Validated) |
| Dibenzo-α-Pyrones (DBPs) | Trace / Unmeasured | 1.5% – 2.5% | > 5.0% Carrier Matrix |
| Water Solubility | Incomplete (Sediment Formed) | 98% Dissolution Rate | 100% Instant Dissolution |
| Heavy Metals (Pb, As, Cd, Hg) | Often Exceeds USP Thresholds | Complies with USP <2232> | Prop 65 Compliant (<0.5 ppm Pb) |
| Primary B2B Application | Traditional Tinctures / Crude Paste | Capsules, Tablets, Premixes | Functional Beverages, Stick Packs, Nootropics |
How consumer demand for vitality, anti-aging, and sports recovery is re-shaping contract manufacturing requirements worldwide.
Traditional raw resin requires messy spoons and warm water preparation, which creates usage friction for modern consumers. Bulk buyers are rapidly pivoting to single-serve liquid stick packs (such as Shilajit blended with organic mountain honey) and micro-encapsulated water-soluble powders for instant beverage stick packs. OEM paper tube packaging adds premium retail positioning while maintaining moisture barriers.
Standalone ingredients face pricing pressure on major marketplaces like Amazon. High-growth brands are ordering custom contract formulations combining High-Yield Shilajit Extract with KSM-66/Sensoril Ashwagandha, Coenzyme Q10, and Cordyceps. This creates multi-pathway male performance, mitochondrial energy, and testosterone-support supplement lines with higher profit margins.
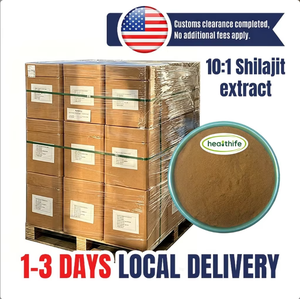
Lead times and supply chain bottlenecks are major risks for scaling brands. Leading Chinese manufacturers are establishing strategic overseas fulfillment nodes. Offering USA Warehouse Stocking with pre-cleared customs allows brand owners to execute just-in-time inventory replenishment, reducing safety stock carrying costs while maintaining domestic delivery speeds.
Procurement teams are actively consolidating vendor lists. Working with a single primary manufacturer that handles raw material purification, custom encapsulation, label compliance design, in-house printing, and high-speed bottling eliminates handoff mistakes, shrinks time-to-market by 4 to 6 weeks, and simplifies QA audit trails.
Engineered for cleanlabel compliance, trace-element preservation, and massive industrial output.
Direct collection of raw mineral pitch from high-altitude rock veins. Incoming shipments are placed in environmental quarantine while undergo initial identity testing, moisture control analysis, and micro-screening before entering processing.
Utilizing pure reverse-osmosis (RO) water without toxic solvents (methanol, acetone, or hexane). Continuous low-temperature counter-current extraction concentrates fulvic acid while maintaining DBP molecular integrity.
Advanced centrifugal separators and selective ion-exchange filtration remove insoluble silica, heavy metals (Pb, As, Cd, Hg), and environmental residues to meet stringent EU food safety and US FDA dietary supplement limits.
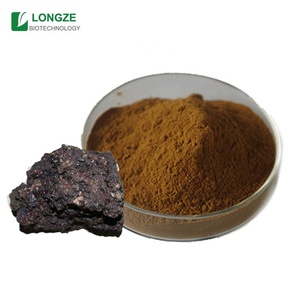
Liquid extracts are either carefully vacuum-concentrated into thick, high-viscosity mineral resin (75%-80% solids) or spray-dried under low temperature into fine 80-mesh, 100% water-soluble dark brown Shilajit powder.
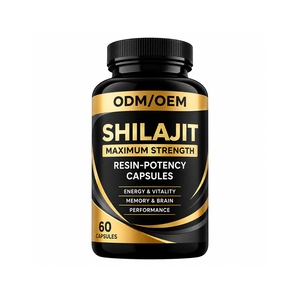
Cleanroom Class 100,000 automated encapsulation lines fill vegetarian (HPMC) or gelatin capsules at 5.5M units per day. Automated honey stick filling and bottle packaging lines handle high-volume retail orders.
Every finished production batch is issued a comprehensive CoA detailing assay percentages (Fulvic Acid by HPLC), physical properties, heavy metal ICP-MS quantification, and total aerobic microbial counts.
Expert answers regarding minimum order quantities, testing protocols, custom formulations, and global export compliance.
Whether you require industrial drum quantities of 50% Fulvic Acid extract powder, ready-to-label Shilajit capsules, or custom OEM honey stick packs, our engineering team is ready to support your supply chain.