Explore our top-tier export-grade raw materials and private-label formulations manufactured under strict NSF/ANSI 455-2 GMP and FDA registered environments.
In the rapidly maturing global dietary supplement ecosystem, procurement officers, brand owners, and contract manufacturers face unprecedented quality scrutiny. As search engines prioritize high Information Gain and validated technical expertise, sourcing standard raw materials is no longer sufficient. Enterprise buyers require advanced custom premixing strategies that solve fundamental pharmaceutical challenges: batch-to-batch content uniformity, active compound degradation, physical particle segregation, and precise bioaccessibility.
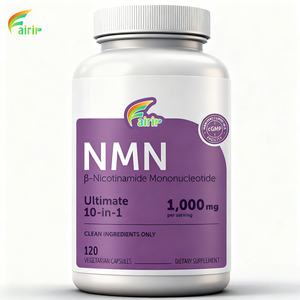
Nicotinamide Mononucleotide is a naturally occurring nucleotide formed by the reaction between a nucleoside containing ribose and nicotinamide. At the cellular level, NMN serves as the immediate direct precursor to Nicotinamide Adenine Dinucleotide (NAD+), a crucial coenzyme involved in mitochondrial ATP generation, PARP-mediated DNA repair, and Sirtuin (SIRT1-7) deacetylase activation.
From a manufacturing standpoint, standard chemical synthesis often leaves trace organic solvents, enantiomeric impurities (such as the biologically inactive Alpha-isomer), and heavy metal residues. Leading Chinese custom premix exporters have revolutionized this landscape by adopting industrial-scale fully enzymatic catalysis processes. This biomimetic synthesis yields pure Beta-NMN (≥99.5%) with 100% enantiomeric purity, zero toxic solvent residues, and dramatically improved thermal stability.
E-E-A-T Quality Insight: When auditing NMN suppliers, demand high-resolution 1H-NMR spectrum analysis alongside LC-MS/MS data to verify the absence of Alpha-NMN isomers. Biologically, only the Beta-anomer (CAS 1094-61-7) fits the active enzyme pocket of NMNAT (nicotinamide mononucleotide adenylyltransferase) to generate NAD+.
Blending pure NMN powder into multi-ingredient longevity matrixes—combining compounds like Trans-Resveratrol, PQQ (Pyrroloquinoline Quinone), Pterostilbene, and Coenzyme Q10—presents severe physical engineering obstacles. Raw ingredient powders vary dramatically in bulk density (0.25 g/mL to 0.75 g/mL) and particle size distribution (40 mesh to 300 mesh). Without advanced physical processing, vibration during transit causes particle segregation, leading to severe dosage variation across encapsulated lots.
To ensure strict USP <905> Uniformity of Dosage Units, our manufacturing infrastructure employs specialized micro-encapsulation and wet-granulation technologies:
Integrating world-class R&D with mass-production capacity to deliver compliant, scalable, and market-ready dietary solutions.
Our green enzymatic reaction tanks operate under strict temperature control, producing pure Beta-NMN powder with purity exceeding 99.5%, low moisture (<1.0%), and heavy metals strictly under 1 ppm.
Manufactured in facilities audited against stringent NSF/ANSI 455-2 dietary supplement cGMP guidelines. Full cGMP batch records (BPR), Certificate of Analysis (CoA), and allergen controls accompany every single shipment.
Equipped with modern automatic high-speed encapsulation machines capable of producing up to 5.5 million hard capsules daily (Vegetable HPMC & Gelatin, sizes 00#, 0#, 1#) with tight weight variance management.
Complete turn-key solutions including custom bottle mold design, HDPE/PET bottle packaging, blister sealing, induction foil sealing, full-color label printing, and retail carton assembly.
Experienced formulation scientists standing by to formulate custom anti-aging, cellular health, sports nutrition, and cognitive enhancement premixes tailored to regional regulatory requirements.
Proven track record of exporting to North America, Europe, Australia, and Southeast Asia. Complete documentation packages including Certificate of Free Sale, Halal, Kosher, and ISO22000 certifications.
Evaluating raw material suppliers requires clear benchmark analysis. The table below illustrates the technical operational gaps between direct top-tier Chinese custom premix manufacturers and typical trading brokers.
| Evaluation Parameter | Top China Direct Factory (Our Standard) | Standard Trading Intermediary | Impact on Brand Owner |
|---|---|---|---|
| Synthesis Technology | Biomimetic Enzymatic Catalysis (≥99.5% Beta) | Chemical Synthesis / Mixed Sources | Higher bioavailability, lower toxicity, zero organic solvents. |
| Quality Assurance | In-house HPLC, LC-MS, ICP-MS Heavy Metal Testing | Outsourced or Batch Copy CoAs | Guaranteed compliance during FDA & Amazon audits. |
| Particle Granulation | Fluidized bed micro-encapsulation & custom mesh (80-200) | Standard raw powder (high segregation risk) | Consistent capsule filling weight and no active ingredient settling. |
| Minimum Order Quantity | Flexible (1kg raw powder / 500 bottles custom) | Rigid broker minimums or broker repackaging | Lower capital requirement for rapid market validation. |
| Traceability & Audit | Complete cGMP Batch Production Records & Factory Visits | No direct facility access; hidden supply chains | Total transparency and supply chain risk mitigation. |
| Lead Time | 3-5 Days Stock Dispatch; 14 Days Custom Formulation | 3-6 Weeks depending on sub-supplier queue | Accelerated time-to-market and seamless inventory flow. |
As the global market for longevity, anti-aging, and metabolic wellness matures, procurement leaders must anticipate key technological shifts driving the dietary supplement industry over the next decade.
Single-ingredient NMN formulations are rapidly evolving into multi-target cellular premixes. Procurement intent is shifting toward synergistic matrixes that combine NAD+ precursors with Sirtuin activators (e.g., Fisetin, Spermidine, Trans-Resveratrol) and NAD+ consumption inhibitors (such as CD38 inhibitors like Apigenin). Custom premix suppliers capable of homogeneously blending these distinct bio-actives without chemical interaction hold a clear competitive advantage.
Global regulatory bodies, including the US FDA and European EFSA, continue to tighten restrictions on residual organic solvents (such as dichloromethane and methanol) in imported health ingredients. The industry is moving decisively toward solvent-free enzymatic bio-catalysis processes. Exporters utilizing renewable enzyme catalysts and closed-loop water purification systems reduce environmental footprint while supplying pure, clean-label raw materials.
With high-speed automated capsule filling machines operating at speeds up to 150,000 capsules per hour, mechanical powder behavior dictates production efficiency. Modern suppliers are investing heavily in particle engineering—tailoring bulk density, tapped density, flowability (Carr's Index), and particle size distribution to prevent bridging, capping, and weight variation on client packaging lines.
In response to stricter retailer intake protocols (e.g., Amazon Supplement Verification Policies, NSF, USP, and Eurofins testing mandates), leading Chinese exporters now provide batch-specific QR-coded Certificates of Analysis backed by independent ISO 17025 accredited laboratory testing.
Comprehensive technical and commercial answers to simplify your import and contract manufacturing process.
Whether you require bulk 99.5% enzymatic Beta-NMN, custom micro-granulated premixes, or turn-key private label capsule production, our technical sales engineers are ready to assist with formulation, sampling, and pricing.