Engineered for maximum bio-solubility, rapid muscle protein synthesis, clean sensory profiles, and strict international compliance.
Insights into macro-nutritional formulation standards, precise micro-milling technologies, and the rising global demand for Japanese manufactured functional proteins.
Japan’s food science infrastructure is universally respected for enforcing some of the strictest purity and sensory thresholds in the global nutraceutical industry. In the bulk protein manufacturing ecosystem, achieving an optimal balance between PDCAAS (Protein Digestibility-Corrected Amino Acid Score) and organoleptic neutralization is critical. Japanese food processors utilize advanced low-temperature enzymatic hydrolysis and ultrasonic deaeration to eliminate off-notes inherent to botanical proteins such as soy, pea, and potato, without compromising peptide integrity.
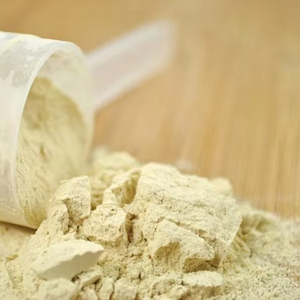
For international buyers importing from Japan, this translates to bulk protein isolates and hydrolysates that exhibit extraordinary solubility, low foam creation, and zero chalkiness—enabling seamless incorporation into high-end ready-to-drink (RTD) beverages, pouch gels, and nutritional supplements.
The global dietary market is transitioning rapidly from basic macronutrient supplementation toward targeted biological functionality. Japanese manufacturing facilities lead this shift by commercializing low-molecular-weight oligopeptides. By subjecting non-GMO soy and pea proteins to controlled endo-peptidase cleavage, our factories produce bioactive peptides (< 1,000 Daltons) that pass directly through the intestinal epithelium into circulation.
These specialized peptides act as potent signal molecules for muscle tissue repair, cellular antioxidant upregulation, and skin matrix elasticity. Furthermore, hypoallergenic alternatives such as 90% Potato Protein Isolate provide food engineers with exceptional gelation and foaming functionality, serving as high-performance, gluten-free egg-white replacements in commercial bakery and processed vegan lines.
Discover how our raw bulk protein materials drive commercial innovation across diverse retail sectors in Japan, East Asia, and global supply chains.
In Japan’s densely populated urban centers, ready-to-drink functional beverages sold across convenience store networks demand total clarity and heat stability during retort sterilization. Our Clear Hydrolyzed Whey Protein Isolate remains completely transparent in acidic pH environments (pH 2.8–3.6) without precipitating out of solution during thermal processing.
Addressing Japan’s super-aging demographic requires specialized enteral nutrition and sarcopenia-prevention powders. Our fast-dissolution adult whey powders and non-gmo soy peptides are incorporated into soft gel foods, medical sachet drinks, and Senior FOSHU (Foods for Specified Health Uses) products tailored for rapid gastrointestinal absorption.
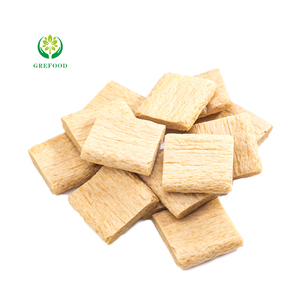
Our high-density Textured Soy Protein (TVP) is engineered with uniform fibrous alignment, mimicking the exact muscle bite of beef and pork. Exported across Southeast Asia under strict HALAL compliance, this ingredient serves as the structural backbone for commercial plant-based dumplings, meatball snacks, and canned vegan foods.
Cross-fit centers and elite athletic training facilities across APAC utilize our instantized, lecithin-coated Whey Isolate and Creatine formulations. Free from artificial fillers, these powders disperse completely in cold water in under 5 seconds using standard shaker bottles, delivering 24g of pristine protein per scoop.
Nutritional inner-beauty drinks in Tokyo and Seoul leverage our bio-fermented Pea Protein Peptides to stimulate dermal fibroblast activity. Exhibiting high radical-scavenging activity and rich in glutamic acid, these micro-peptides support skin hydration and collagen synthesis from within.
Combining state-of-the-art cleanroom automated blending, rigorous raw-material identity testing, and end-to-end export documentation.
Referencing industry-leading production standards, our processing plant integrates full-cycle contract manufacturing under one roof. We manage ingredient sourcing, custom formulation engineering, high-shear micro-blending, automated capsule filling, powder pouching, and rigid bottling.
Operating in an NSF/ANSI 455-2 GMP certified and FDA-registered facility, our production lines achieve a daily throughput capacity exceeding 5.5 million capsules and tens of metric tons of micro-milled powder. By eliminating third-party handoffs, we eliminate vendor ping-pong, compress manufacturing lead times by weeks, and safeguard your proprietary intellectual property.
Quality isn't self-declared; it is scientifically proven. Every single raw material lot entering our warehouse is immediately quarantined and subjected to stringent identity verification. Finished batches undergo comprehensive chemical, physical, and microbiological screening before release.
Our analytical laboratory suite utilizes High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Atomic Absorption Spectroscopy to guarantee potency, verify heavy metal clearance (Lead, Arsenic, Cadmium, Mercury), and confirm zero microbial contamination.
Essential guidance on Minimum Order Quantities (MOQs), export logistics, custom flavor matching, and regulatory compliance.
For our standard market-ready bulk raw materials (such as 90% Soy Protein Isolate or Whey Protein Concentrate in 25kg industrial drums), MOQs start at 500 kg to 1 Metric Ton. For custom contract formulations, bespoke flavor creation, or branded retail container runs, our MOQs typically begin at 1,000 units for powders and 5,000 units for custom encapsulated SKUs. Low-volume validation runs can be arranged for strategic brand launches.
Our in-house R&D team specializes in sensory neutralization and natural flavor matching (including Matcha, Double Rich Chocolate, Vanilla Bean, and Japanese Yuzu). We utilize fluid-bed agglomeration and non-GMO sunflower lecithin coating to ensure powders achieve instant dispersibility in ambient and cold liquids without clumping.
As a premier Japanese exporter, we supply comprehensive compliance packages for smooth customs clearance worldwide. This includes Certificates of Analysis (CoA), Manufacturer Certificates, Health Certificates, Non-GMO Statements, Allergen Declarations, HALAL Certifications, and Free Sale Certificates compliant with FDA, EU, and Southeast Asian food safety authorities.
Yes. Our manufacturing facility operates strictly segregated processing zones with isolated air filtration (HEPA) systems to prevent cross-contamination. Detailed sanitation protocols and cleaning validation swabs (ATP and ELISA testing) are conducted between production cycles to guarantee allergen purity for vegan and dairy-free lines.
Standard raw material bulk supply orders are typically dispatched within 7–14 working days. Custom OEM/ODM manufacturing projects—inclusive of custom flavor lab trials, label artwork compliance review, micro-milling, blending, and quality release—average 4 to 6 weeks from final purchase order and artwork sign-off.
Industrial buyers and brand procurement officers can request raw material samples (typically 100g to 500g trial packs) along with full technical data sheets (TDS) and CoAs directly through our global live chat portal. Click the "Get Catalog" button anywhere on this page to initiate an immediate inquiry with our technical sales engineers.
Partner with Japan's leading bulk protein factory. Access market-ready formulas, custom high-purity isolates, and complete turnkey export support today.
Get Catalog