Market-ready formulas engineered for maximum solubility, bio-availability, and regulatory compliance in North America.
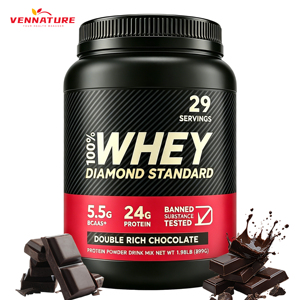
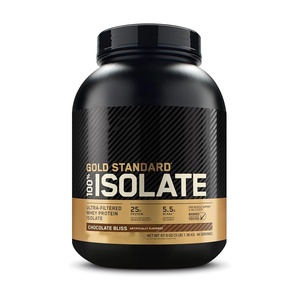
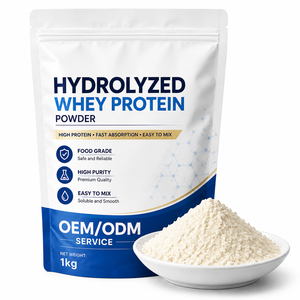
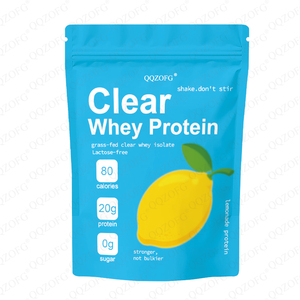
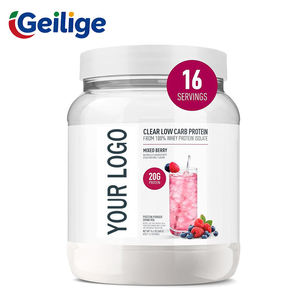
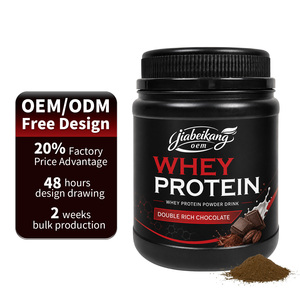
The United States sports nutrition and dietary supplement ecosystem represents the largest, most sophisticated consumer market globally. For American supplement brand owners, contract distributors, Amazon FBA sellers, and institutional health procurement teams, securing a resilient, high-purity, cost-effective protein source is fundamental to enterprise growth. Partnering directly with a premier China wholesale whey protein factory offers exceptional margin elasticity and advanced processing capabilities, provided the partner demonstrates flawless adherence to US regulatory mechanisms.
Historically, cross-border ingredient sourcing presented friction regarding regulatory scrutiny, lot consistency, and logistics verification. Today, high-capacity Chinese manufacturing hubs operate state-of-the-art ceramic membrane filtration systems, automated instantization suites, and fully integrated ISO-17025 laboratory testing. By aligning China’s massive manufacturing output with North American market specifications—such as FDA 21 CFR Part 111 cGMP standards, NSF/ANSI 455-2 compliance, and California Proposition 65 heavy metal thresholds—leading suppliers have built a seamless operational bridge to the US market.
This whitepaper delivers an exhaustive breakdown of processing technologies, localized market demands in the United States, intent-driven consumer segmentation, regulatory compliance pathways, and private label execution frameworks designed to maximize Information Gain for procurement decision-makers.
Whey protein is no longer restricted to traditional bodybuilders drinking post-workout shakes. The modern American consumer landscape spans multiple demographic cohorts, demanding tailored physical properties, particle mesh sizes, instantization levels, and macro profiles. China-based custom manufacturing provides precise ingredient engineering matched to these distinct US application scenarios:
Targeted at hardcore fitness enthusiasts, crossfitters, and collegiate athletes. Formulations emphasize high Branched-Chain Amino Acid (BCAA) content, specifically Leucine ratio fortification, combined with rapid-absorbing Whey Protein Hydrolysate (WPH) and Isolate (WPI) for rapid muscle protein synthesis (MPS).
A massive growth vector in North America. Clear Whey Isolate utilizes ultra-low pH acidification and specialized enzymatic processing to achieve complete optical clarity when dissolved in water, providing a refreshing, juice-like mouthfeel with zero milky residue and zero sugar.
Formulated for the American Baby Boomer demographic. Low-lactose, easily digestible Whey Isolate fortified with digestive enzymes (Protease, Lactase), Vitamin D3, Calcium, and Electrolytes to combat age-related muscle wasting (sarcopenia) and enhance mobility.
Zero-added-sugar, ultra-low carbohydrate matrix incorporating clean fats (such as Coconut-derived MCT Oil powder) paired with cold-filtered Whey Protein Isolate. Engineered to maintain metabolic ketosis while fulfilling daily macros.
Heat-stable, non-denatured Whey Protein Concentrate (WPC80) engineered with specific gelling and emulsification properties. Designed for commercial US bakeries, high-protein pancake mixes, protein bars, and functional snack formulations.
To gain a competitive edge in search rankings and market share, US supplement brands must align product developments with real-time consumer intent trends. According to recent North American market research, consumer preferences have shifted dramatically from basic protein content to holistic product integrity:
| Whey Grade | Protein Concentration | Lactose Profile | Fat / Ash Content | Primary US Target Application |
|---|---|---|---|---|
| Whey Protein Concentrate (WPC80) | 78.0% - 82.0% | 4.0% - 8.0% | 5.0% - 7.0% | Mass Gainers, Functional Bakery, Budget Sports Shakes |
| Whey Protein Isolate (WPI90) | 90.0% - 92.5% | < 0.5% (Virtually Zero) | < 1.0% | Lean Muscle Synthesis, Keto, Lactose-Intolerant Formulas |
| Hydrolyzed Whey (WPH) | 85.0% - 90.0% | < 1.0% | < 1.5% | Clinical Nutrition, Intra-Workout, Rapid Peptide Delivery |
| Clear Whey Isolate | 88.0% - 91.0% | 0.0% | 0.0% | Juice-Style RTD Mixes, Refreshing Low-pH Hydration Shakes |
Partnering with an elite OEM/ODM factory in China provides American brands with structural cost efficiencies without sacrificing global quality benchmarks. Mirroring top-tier US contract manufacturing standards—such as Utah’s leading dietary supplement facilities—our manufacturing infrastructure operates under stringent quality control protocols:
Equipped with high-capacity V-blenders and ribbon mixers operating inside ISO Class 8 cleanrooms. Capability to produce over 5.5 million powder packaging and encapsulation units daily, ensuring rapid batch throughput during peak retail demand cycles.
Turnkey packaging flexibility including HDPE/PET wide-mouth canisters, flexible multi-layer foil gusset bags, single-serve sachets, and stick-packs. In-house label design, FDA Supplement Facts compliance verification, and high-speed automated shrink-banding.
Proprietary flavor masking technology that eliminates the bitter peptide notes of hydrolyzed protein. Over 115 market-ready, taste-tested flavor matrix profiles ranging from Belgian Chocolate to Cinnamon Cereal Milk, Salted Caramel, and Dragonfruit Lemonade.
Complete documentation packages supplied for every shipment: Certificate of Analysis (CoA), HPLC purity breakdown, Heavy Metal ICP-MS screening, Microbicides/Pathogen clearing, Allergen statements, and Foreign Supplier Verification Program (FSVP) dossiers.
Direct technical answers addressing regulatory compliance, quality control, minimum order thresholds, and supply chain logistics for North American brand owners.
Eliminate middleman markups, secure regulatory-compliant formulations, and access high-capacity wholesale manufacturing tailored to the North American market. Speak directly with our lead formula engineers today.
Inquire Now