High-potency, analytical laboratory-verified dietary supplements manufactured under strict US FDA registration and NSF GMP standards, configured for rapid customs release in Oman.
The Sultanate of Oman is undergoing a profound structural shift in consumer health dynamics. Driven by Oman Vision 2040 initiatives focused on preventative healthcare, lifestyle enhancement, and metabolic wellness, the domestic market for dietary supplements has expanded beyond basic multivitamins into high-specification cellular longevity compounds, specialized anti-aging bio-actives, and high-purity metabolic support formulations. B2B importers, pharmacy conglomerates, and private label wellness brands operating out of Muscat, Salalah, and Sohar face dual imperatives: sourcing high-potency, laboratory-certified formulations while complying strictly with GCC Standardization Organization (GSO) regulations and Ministry of Health (MoH) product clearance protocols.
User intent mining across Middle Eastern healthcare buyers reveals a clear preference for transparency, verifiable efficacy, and climate-resilient packaging. Because Oman experiences ambient outdoor temperatures frequently exceeding 45°C during summer months, supplement capsules must possess exceptional thermal stability and humidity resistance. Brands seeking to capture market share must move away from generic unverified suppliers and align with contract manufacturers that offer certified cGMP compliance, rigorous raw material identity testing, and specialized hard-capsule engineering.
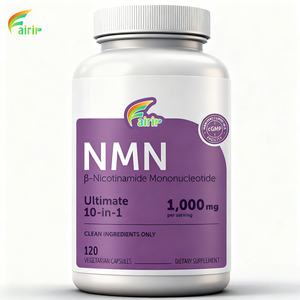
Requires shelf-ready, serialized, high-end packaged NMN and NAD+ capsule SKUs with full Certificates of Analysis (CoA) and heavy metal compliance for seamless MoH clearance.
Demands custom clinical-grade encapsulation featuring targeted cellular repair molecules, vegetarian HPMC shells, and zero artificial excipients for premium patient programs.
Leverages fast-turnaround market-ready formulations (115+ ready formulas) to capture rapidly shifting digital consumer trends across Oman, UAE, and the wider GCC region.
Engineering high-bioavailability capsules optimized for purity, consistency, and global regulatory acceptance.
Our Utah facility utilizes automated tamping-pin and intermittent-motion rotary encapsulation machinery capable of producing up to 5.5 million capsules per day. We maintain precise fill-weight tolerances (±1.5%) across size 00, 0, 1, and 2 capsule shells, eliminating fill weight variation and guaranteeing consistent dosing.
To support the religious and ethical requirements of the Omani population, we offer 100% vegetarian Hydroxypropyl Methylcellulose (HPMC) shells alongside conventional pharmaceutical bovine gelatin capsules. Our supply chain features strict ingredient segregation, zero cross-contamination protocols, and non-GMO, Halal-compatible certification pathways.
Every raw material batch undergoes identity verification via FT-IR, HPLC potency testing, heavy metal screening (ICP-MS for Lead, Arsenic, Cadmium, Mercury), and comprehensive microbiological testing (Salmonella, E. coli, Staphylococcus aureus) before releasing materials to blending.
In hard-capsule dietary supplement manufacturing, ingredient flowability and bulk density dictate dissolution kinetics. For compounds such as 99% Beta-Nicotinamide Mononucleotide (NMN, CAS 1094-61-7) and NAD+ precursor complexes, raw powder micronization is crucial. Our blending facility utilizes precision cone blenders with controlled humidity ambient air systems, ensuring particle size uniformity (typically 80-100 mesh size). This prevents ingredient stratification during encapsulation, guaranteeing that every capsule delivers exact claim potency from the first unit to the last.
Shipping supplements to Middle Eastern destinations like Muscat requires packaging engineered to withstand high ambient moisture and sea transport heat. We utilize high-density polyethylene (HDPE) and UV-blocking amber PET bottles equipped with hermetic foil induction seals, integrated molecular sieve desiccants, and tamper-evident neck bands to safeguard active ingredient integrity over a 24-to-36-month shelf life.
For clinical-grade private label encapsulation, we provide Alu-Alu (aluminum-aluminum) and PVC/PVDC moisture-barrier blister strip packaging. This delivers unit-dose protection against oxygen permeation and hydrolytic degradation—making it ideal for humid coastal regions in Southern Oman such as Salalah.
Combining over 28 years of US contract manufacturing excellence with streamlined export support for international buyers.
Independently audited dietary supplement cGMP facility registration. Our documentation passes strict international regulatory checks without friction.
In-house label design and high-resolution printing. We assist with Supplement Facts layout, multilingual (Arabic/English) formatting, and compliance checks.
Flexible production lines starting from low unit minimums for market-ready SKUs, scaling seamlessly to multi-container custom runs as your brand grows.